Manufacturing in Bekasi, West Java — Indonesia ISO 9001 · IATF 16949 · ISO 14001 · ISO 45001

Micro Screws

Self-Tapping Micro Screws

Thread-forming and thread-cutting screws for plastics and thin sheet metal

Thread formingPlastic & sheet metalSharp thread rootBoss-safe
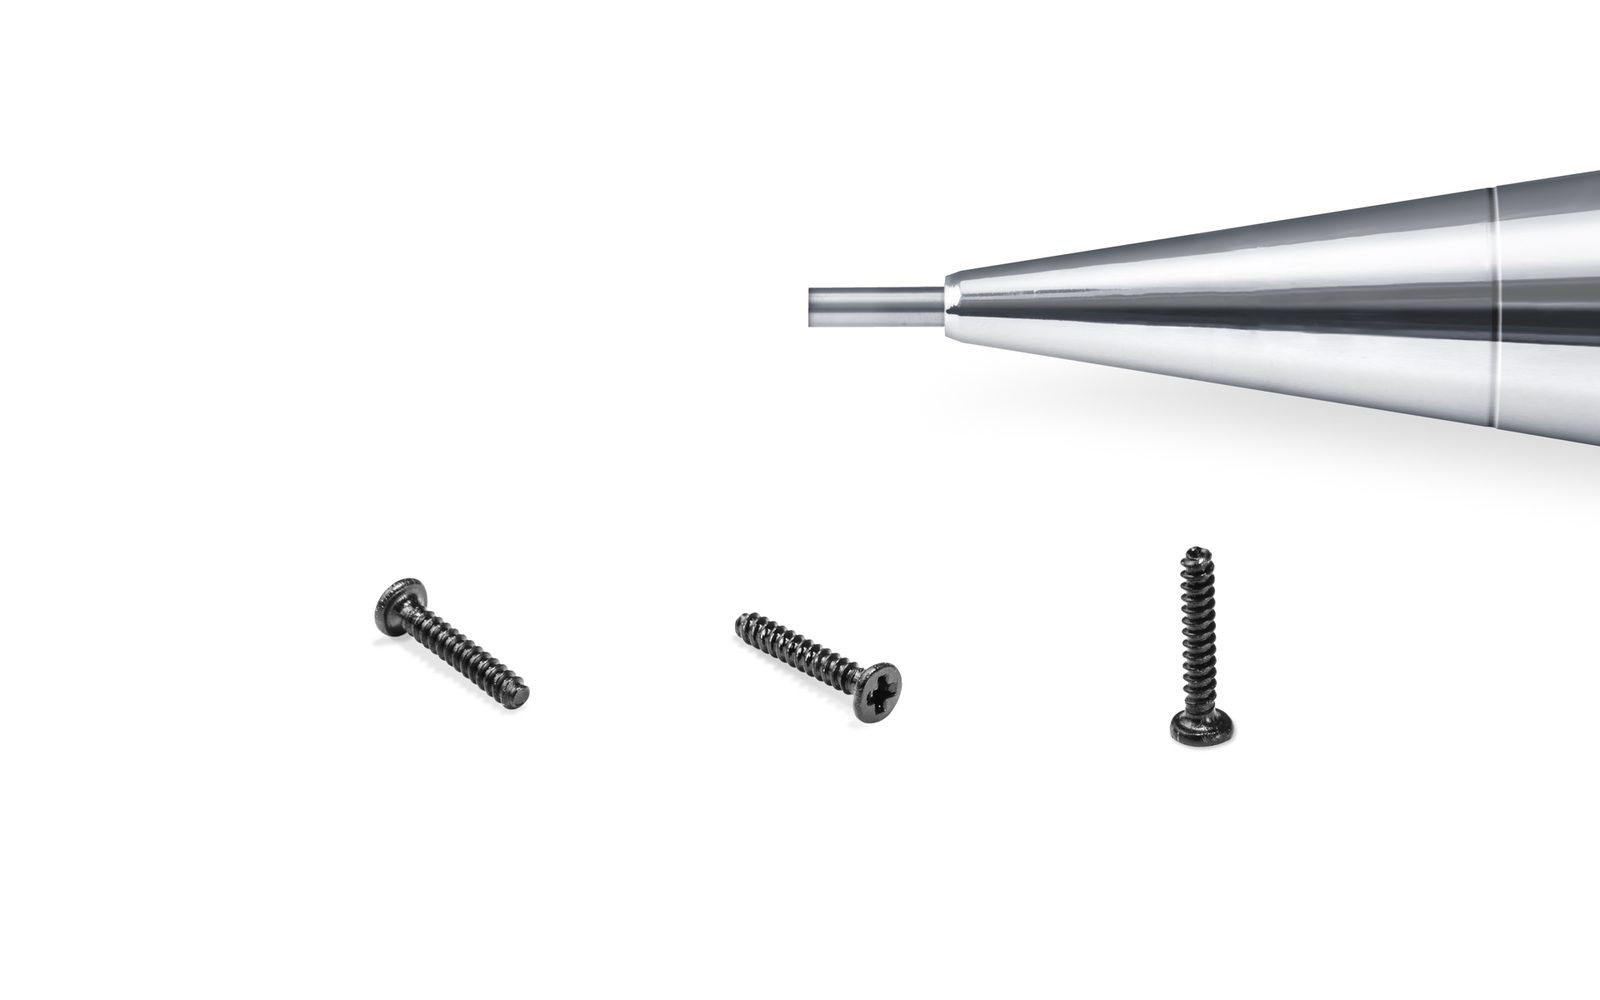
Pan head self-tapping micro screws arranged in a row M0.6 – M4 · Micro Screws

Overview

Self-Tapping Micro Screws from M0.6 – M4

Self-tapping screws remove a process step: no tapping, no inserts, no adhesive. In miniature plastic housings they are often the only practical way to close a part, because the boss wall may be thinner than the insert that would otherwise be required. The trade-off is that the screw now has to cut or form its own thread without splitting the boss, stripping under drive torque or leaving stress marks on a visible surface.

We engineer the point, thread flank and minor diameter together with the boss geometry. For plastics we recommend thread-forming screws with a 30° or 45° point and a relatively large minor diameter, paired with a boss diameter of roughly 1.8–2.2× the screw diameter. For thin sheet metal we produce thread-cutting screws with a slotted or slotted-point tip that clears the chip. Both types are available with undercut heads for flush seating in soft material.

Diameter range

M0.6 – M4

Types

Thread-forming (plastic), thread-cutting (sheet metal)

Point styles

30° / 45° cone, blunt, slotted, slotted-point (Type 23 / Type 25)

Length range

2.0 mm – 40 mm

Length tolerance

±0.10 mm

Recommended boss Ø

1.8 – 2.2 × screw diameter

Design intent

What this product solves

Six engineering decisions that separate a micro fastener that works from one that merely fits the drawing.

Point geometry matched to the boss

Point angle, tip relief and thread start are tuned to the boss diameter and resin so the screw starts straight and forms rather than tears the thread.

Crack-resistant thread form

A wider root radius and controlled flank angle reduce hoop stress in glass-filled nylon and polycarbonate bosses.

Undercut head option

An undercut beneath the head captures displaced plastic, letting the head seat flush without a visible witness ring.

Thread-cutting for sheet metal

Slotted and slotted-point tips cut a clean thread in 0.4–1.2 mm steel and aluminium sheet with minimal deformation.

Drive torque matched to resin

We publish recommended driving and stripping torque per size and material so your assembly line can set the driver clutch correctly.

Colour-matched heads

Painted or PVD-coated heads can be matched to the housing colour where the fastener is visible on the product exterior.

Technical data

Recommended pilot hole and boss diameter for thread-forming screws in plastics

Reference data for design and sourcing. For a specific part, the drawing governs — these tables are the starting point for a joint review.

SizePilot hole (mm)Boss Ø (mm)Drive torque (N·m)Strip torque (N·m)Typical use
M0.60.45 – 0.501.20.020.04Micro speaker grilles
M0.80.60 – 0.661.50.040.08Earbud housings
M1.00.75 – 0.821.90.070.13Wearable cases
M1.20.90 – 0.982.30.110.20Camera housings
M1.41.05 – 1.152.70.160.28Small appliance shells
M1.61.20 – 1.303.00.220.40Notebook bezels
M2.01.50 – 1.623.80.400.75Router and hub cases
M2.51.88 – 2.004.80.751.40Control boxes
M3.02.25 – 2.405.81.302.40Appliance panels
M4.03.00 – 3.207.62.805.00HVAC covers

Values are typical for the stated material and finish. Actual performance depends on the mating material, engagement length and assembly torque. Confirm with a sample test before design freeze.

Options

Heads, drives, materials and finishes

Mix these within one part number family. Where a combination is not manufacturable at your tolerance, we will say so at quotation rather than after the first lot.

Head styles

  • Pan head — Standard for plastic housings, good load spread
  • Flat head — Flush finish where the screw is visible
  • Oval head — Decorative flush look, common on consumer devices
  • Binding head — Undercut for thin panels and wire clamping
  • Hex washer head — Sheet metal and bracket fixing

Drive types

  • Phillips
  • Pozidriv
  • Torx
  • Torx Plus
  • Hex socket
  • Square drive

Materials

  • Case-hardened carbon steel (SWCH18A)
  • SUS304 stainless
  • SUS410 hardened stainless
  • C3604 brass
  • Aluminium 5056 (colour anodised)

Finishes

  • Zinc trivalent clear / blue
  • Black oxide
  • Electroless nickel
  • Painted head (colour matched)
  • PVD TiN / black DLC
  • Passivation (stainless)

Where it is used

Typical applications

Representative positions rather than an exhaustive list. Many of our parts are designed for one specific assembly and never appear in a catalogue.

Application reference by assembly position
Assembly Typical use
Earbuds and hearables M0.6–M0.8 thread-forming screws into PC/ABS shell halves
Smart speakers M1.6–M2.0 screws into glass-filled nylon bosses
Notebook bottom covers M2.0 thread-forming screws with low-head profile
Router and set-top boxes M2.5–M3.0 screws into moulded ABS posts
Sheet metal brackets M3.0–M4.0 thread-cutting screws in 0.8–1.2 mm CRS
Robot cosmetic covers M2.0 colour-matched screws on external shells

Quality control

What we measure on every lot

Inspection is not a final gate. It is a set of checks placed where a process can actually drift, with the result recorded against the lot code.

01

Point angle and tip concentricity, optical comparator

02

Thread profile, toolmaker microscope

03

Driving and strip torque, torque tester on production resin

04

Boss crack inspection after drive, 20× magnification

05

Head diameter and undercut depth

06

Hardness, HV 0.3

07

Coating thickness, X-ray fluorescence

08

Salt spray where corrosion resistance is specified

Questions

About self-tapping

The questions our engineers answer most often on this product family.

Still deciding? Send the assembly drawing and the service condition. We will recommend a size, finish and locking method — and tell you if a different product family is the better answer.
Thread-forming or thread-cutting for my plastic part?
Thread-forming is the default for thermoplastics because it cold-flows material around the screw and produces a stronger joint. Thread-cutting is used for brittle or very glass-filled resins where forming stress would crack the boss, and for thermosets.
How many times can a self-tapping screw be re-used?
In unfilled resin, 3–5 cycles are typical before strip torque drops noticeably. In glass-filled resin, plan for 1–2 cycles. If the product will be serviced repeatedly, specify a machine screw with a threaded insert instead.
Why do my bosses crack during driving?
The three usual causes are an undersized pilot hole, a boss wall thinner than about 0.6× the screw diameter, or moulded-in stress from a cold gate. Send us the boss drawing and resin grade and we will recommend a pilot diameter and point style.
Can you supply screws that match the housing colour?
Yes. Painted heads and PVD colours can be matched to a Pantone or moulded chip. Colour matching is done on the head only; the thread remains uncoated to protect the formed thread.

Related products

Often specified together

These families are frequently used in the same assembly, or as an alternative when the joint requirement changes.

M0.8 machine thread micro screws shown beside a pencil tip for scale

Micro Screws · M0.5 – M6

Machine Thread Micro Screws

Precision machine screws from M0.5 to M6 with rolled Class 6g threads, tight head concentricity and clean drive recesses for automated driving.

Class 6g threadRolled threadStainless / carbon steel
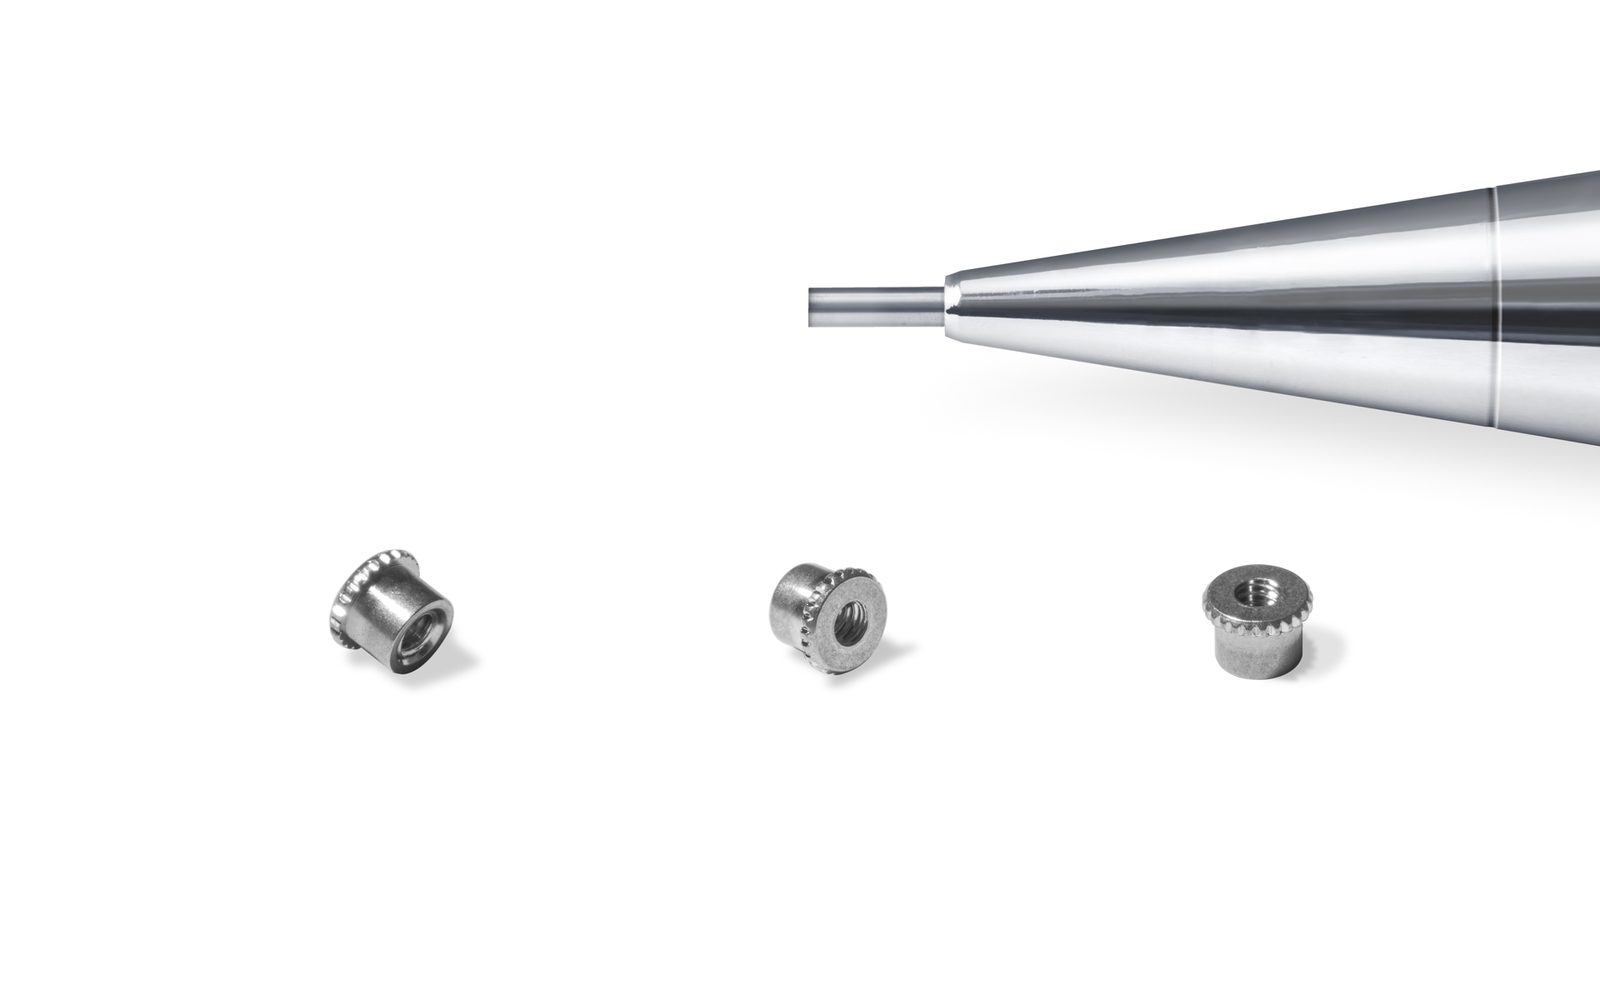
Brass threaded inserts for plastic housings

Precision Components · M1 – M6

Threaded Inserts

Brass and stainless threaded inserts that give plastic parts a durable metal thread — heat-set, moulded-in, ultrasonic and press-fit versions from M1 to M6.

Heat-setMoulded-inBrass / SS
Micro screws with a blue nylon patch threadlocking element

Micro Screws · M0.8 – M6

Precoated Screws

Screws with a factory-applied locking or sealing element, so the assembly line receives a ready-to-drive fastener with no liquid adhesive and no cure time.

Nylon patchMicro-encapsulated3M tape
Precision stamped metal parts including clips and contacts

Specialties · 0.05 – 1.5 mm strip

Precision Stamped Parts

Progressive-die stamped parts from 0.05 to 1.5 mm strip — contacts, spring clips, EMI shields and mounting brackets produced alongside our screw lines.

Progressive dieIn-die tappingReel or loose

Need self-tapping to your drawing?

Send a drawing or 3D model with the mating material and finish requirement. We reply with a process route, tolerance review and price — usually within two working days.