Micro Screws · M0.5 – M6
Machine Thread Micro Screws
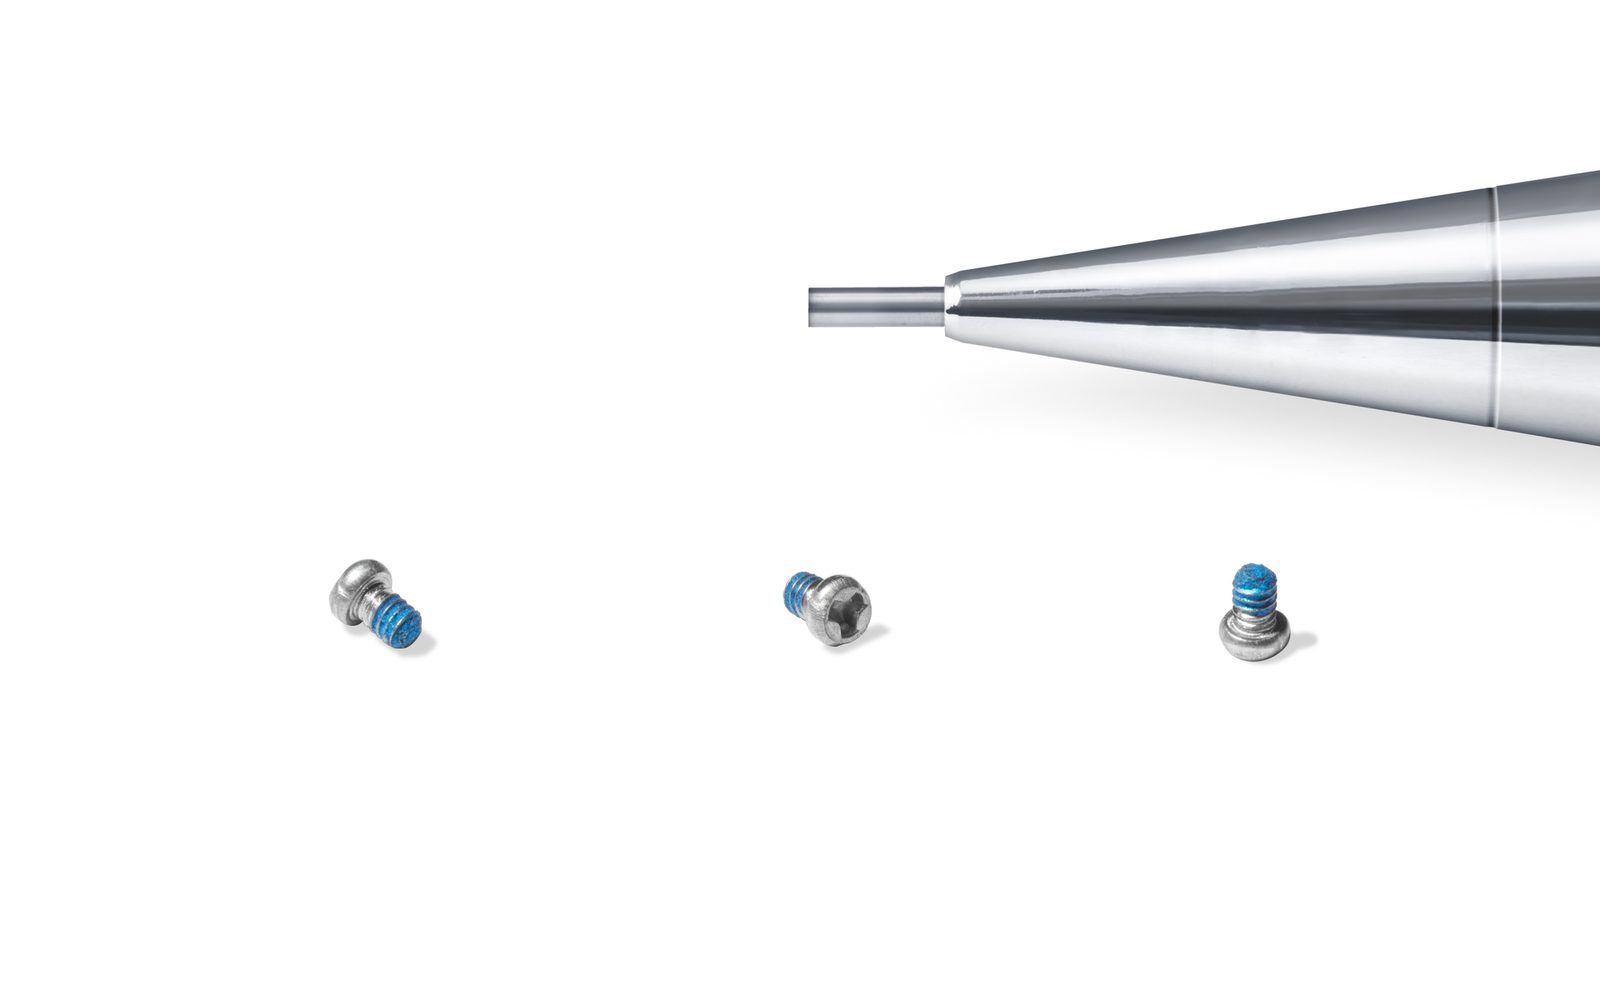
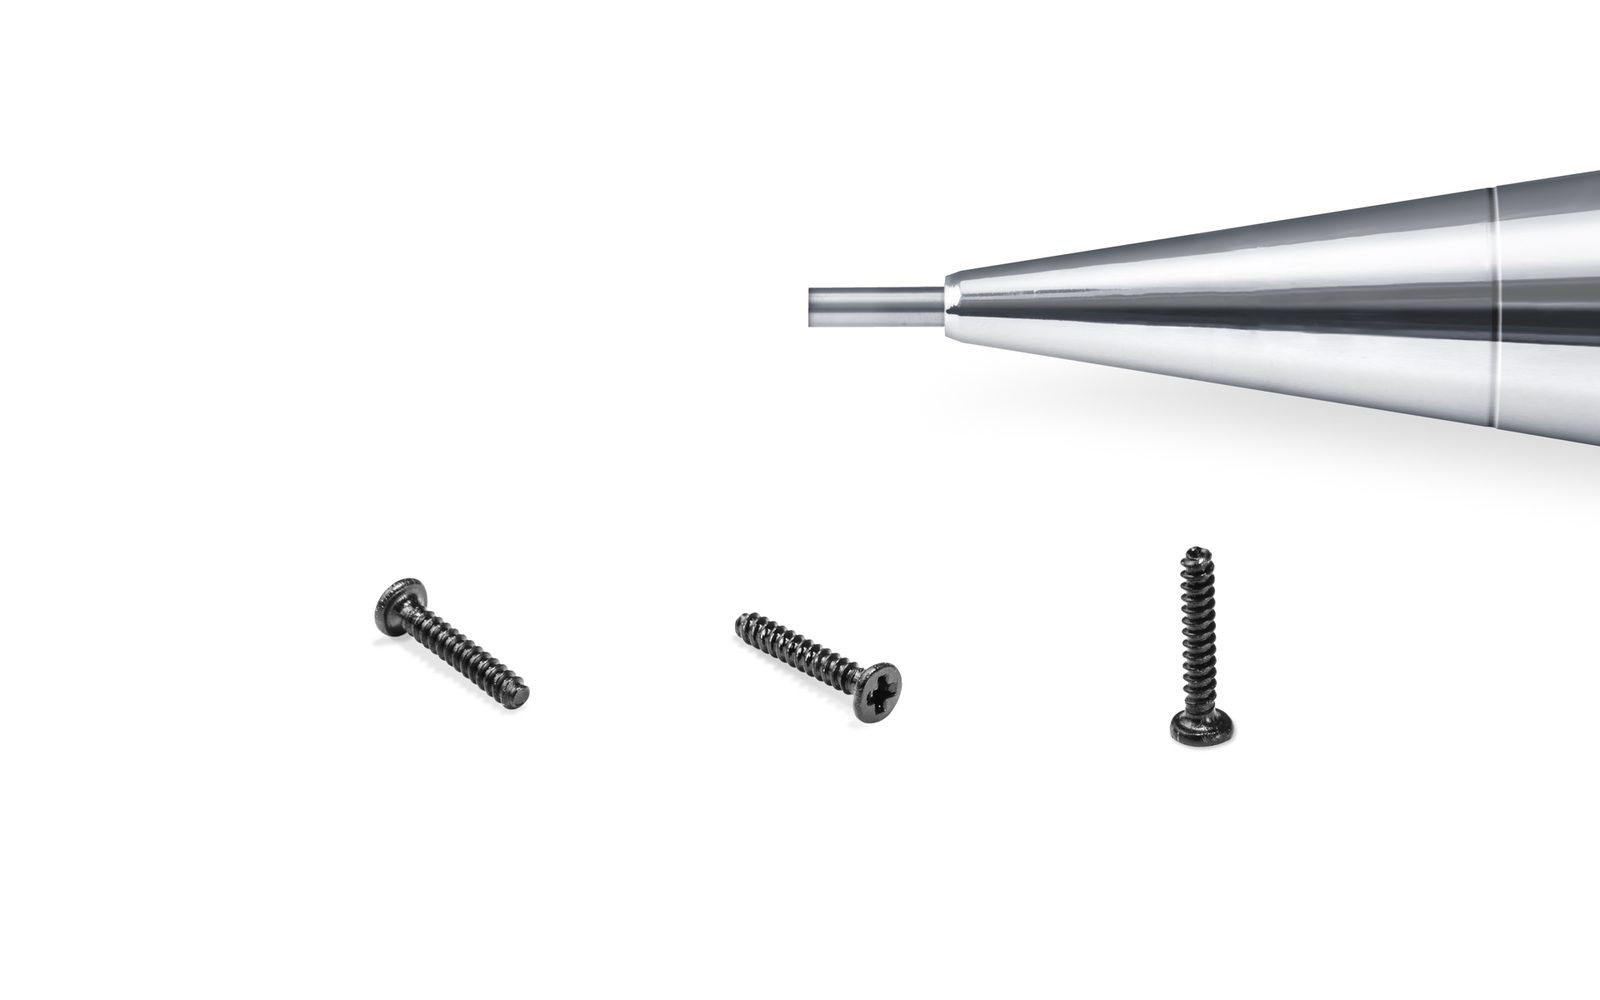
Precision machine screws from M0.5 to M6 with rolled Class 6g threads, tight head concentricity and clean drive recesses for automated driving.
Micro Screws
TiN, CrN, TiCN and DLC coatings for wear resistance and premium finish
M0.8 – M6 · Micro Screws Overview
PVD is not paint and it is not electroplating. A solid coating is vaporised in a vacuum chamber and deposited atom by atom onto the screw, forming a ceramic film 2–5 µm thick that is harder than the tool steel driving it. For micro screws this solves two problems at once: the drive recess stops deforming after a few thousand cycles on the assembly line, and the head can carry a durable decorative finish that electroplating cannot match.
We run multi-arc and magnetron sputtering chambers with fixtures designed for small fasteners, so parts are coated uniformly on the head, recess and thread rather than only on the line of sight. Standard films are TiN (gold), CrN (silver-grey), TiCN (grey-violet), TiAlN (dark grey) and DLC (near-black). Film thickness, adhesion and colour are verified per batch, and we can coat stainless, alloy steel, brass and titanium substrates.
Diameter range
M0.8 – M6
Films available
TiN, CrN, TiCN, TiAlN, DLC, AlCrN
Film thickness
2 – 5 µm (typical 3 µm)
Micro-hardness
HV 1800 – 2500 (TiN / TiCN)
Friction coefficient
0.15 – 0.25 (steel on steel, dry)
Max service temperature
500 °C (TiN) / 400 °C (DLC)
Design intent
Six engineering decisions that separate a micro fastener that works from one that merely fits the drawing.
TiN and TiCN films reach HV 1800–2500, so the recess resists deformation through tens of thousands of automated drive cycles.
The coefficient of friction of a PVD film is roughly half that of untreated steel, giving repeatable torque-to-preload without lubricant.
Gold, black, gunmetal and rainbow finishes are produced without hexavalent chromium or cyanide chemistry.
Rotating fixtures expose the recess and thread flank to the vapour stream, avoiding the shadowing that causes patchy colour on small parts.
Rockwell indentation and scratch testing confirm film adhesion; thickness is measured by X-ray fluorescence and cross-section.
A PVD film over a nickel or CrN interlayer delivers salt spray resistance while keeping the surface hard and slick.
Technical data
Reference data for design and sourcing. For a specific part, the drawing governs — these tables are the starting point for a joint review.
| Film | Colour | Hardness (HV) | Friction | Best for | Max temp |
|---|---|---|---|---|---|
| TiN | Gold | 2300 | 0.20 | General wear resistance, decorative gold | 500 °C |
| CrN | Silver-grey | 1800 | 0.22 | Corrosion resistance, mould release | 400 °C |
| TiCN | Grey-violet | 3000 | 0.18 | High wear, punch and die, driver bits | 450 °C |
| TiAlN | Dark grey | 2800 | 0.25 | High temperature wear | 800 °C |
| DLC | Near-black | 2000 – 4000 | 0.10 | Low friction, black decorative, sliding | 400 °C |
| AlCrN | Grey | 3200 | 0.22 | Extreme abrasive wear | 900 °C |
Values are typical for the stated material and finish. Actual performance depends on the mating material, engagement length and assembly torque. Confirm with a sample test before design freeze.
Options
Mix these within one part number family. Where a combination is not manufacturable at your tolerance, we will say so at quotation rather than after the first lot.
Where it is used
Representative positions rather than an exhaustive list. Many of our parts are designed for one specific assembly and never appear in a catalogue.
| Assembly | Typical use |
|---|---|
| Smartphone exterior screws | Black DLC pentalobe and Torx screws with colour-matched heads |
| Wearable bezels | Gold TiN screws as a visible design detail |
| Robot joint covers | CrN-coated screws resisting repeated driver engagement |
| High-cycle assembly lines | TiCN-coated recesses surviving 50,000+ automated drives |
| Optical instrument housings | Low-outgassing DLC screws near lenses |
| Luxury audio products | Rainbow PVD for a premium exposed-fastener look |
Quality control
Inspection is not a final gate. It is a set of checks placed where a process can actually drift, with the result recorded against the lot code.
01
Film thickness, XRF and cross-section SEM
02
Adhesion, Rockwell C indentation (HF 1–2)
03
Micro-hardness, HV 0.05
04
Colour, spectrophotometer against master chip
05
Friction coefficient, torque-tension test
06
Salt spray, ASTM B117
07
Outgassing, ASTM E595 for optical and space applications
08
Recess fit after coating, go/no-go driver bit
Questions
The questions our engineers answer most often on this product family.
Related products
These families are frequently used in the same assembly, or as an alternative when the joint requirement changes.
Micro Screws · M0.5 – M6
Precision machine screws from M0.5 to M6 with rolled Class 6g threads, tight head concentricity and clean drive recesses for automated driving.
Micro Screws · M0.8 – M6
Screws with a factory-applied locking or sealing element, so the assembly line receives a ready-to-drive fastener with no liquid adhesive and no cure time.
Specialties · M0.8 – M6
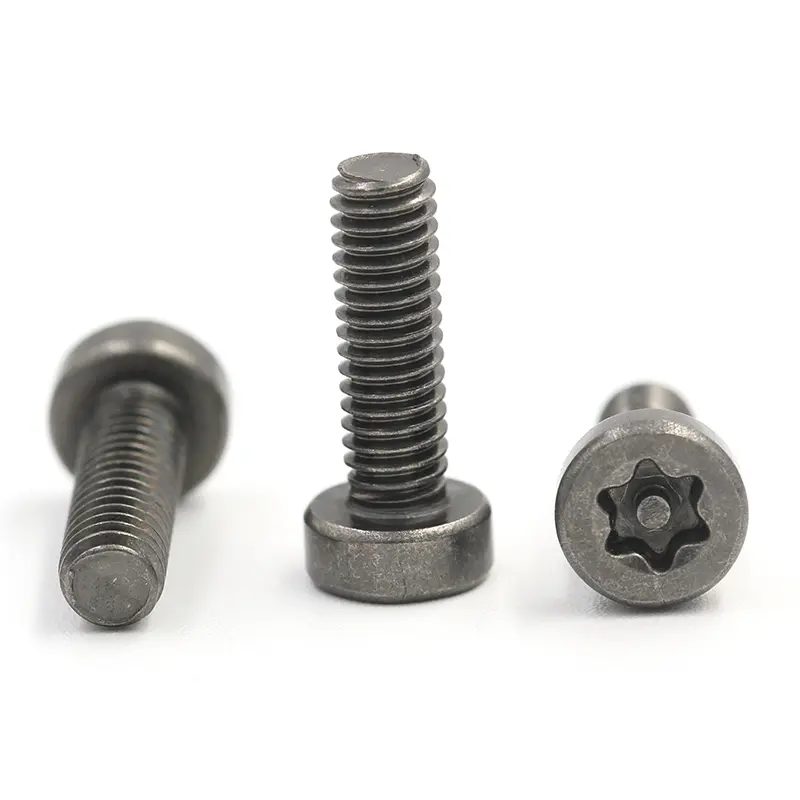
Tamper-resistant micro screws with pin-in-Torx, tri-wing, pentalobe and one-way drives — for products where access must be controlled or evidenced.
Send a drawing or 3D model with the mating material and finish requirement. We reply with a process route, tolerance review and price — usually within two working days.