Company
Plant tour
Nine areas, one continuous route from wire coil to labelled carton. This is what a customer visit actually looks like.
01 / 09
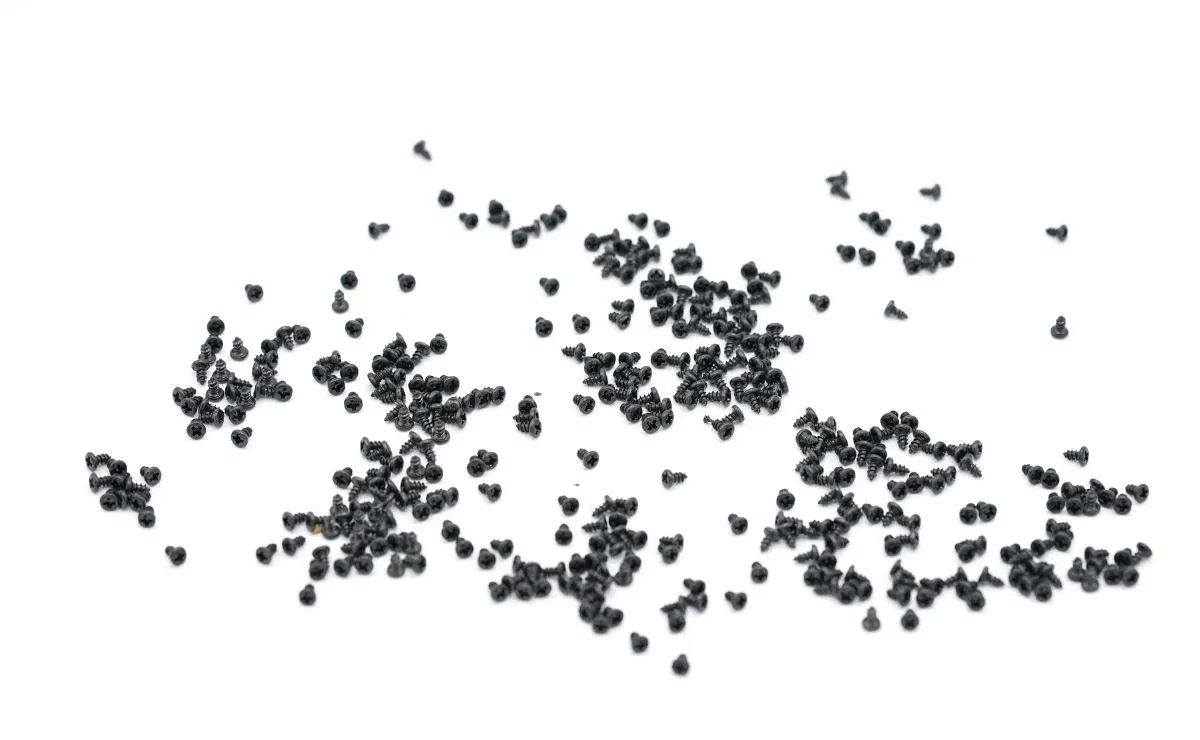
Wire intake and verification
Every coil is checked for diameter, ovality, surface defects and hardness before release to production. The heat number is recorded and becomes the first link in the lot traceability chain.
Incoming inspection · heat number recorded
02 / 09
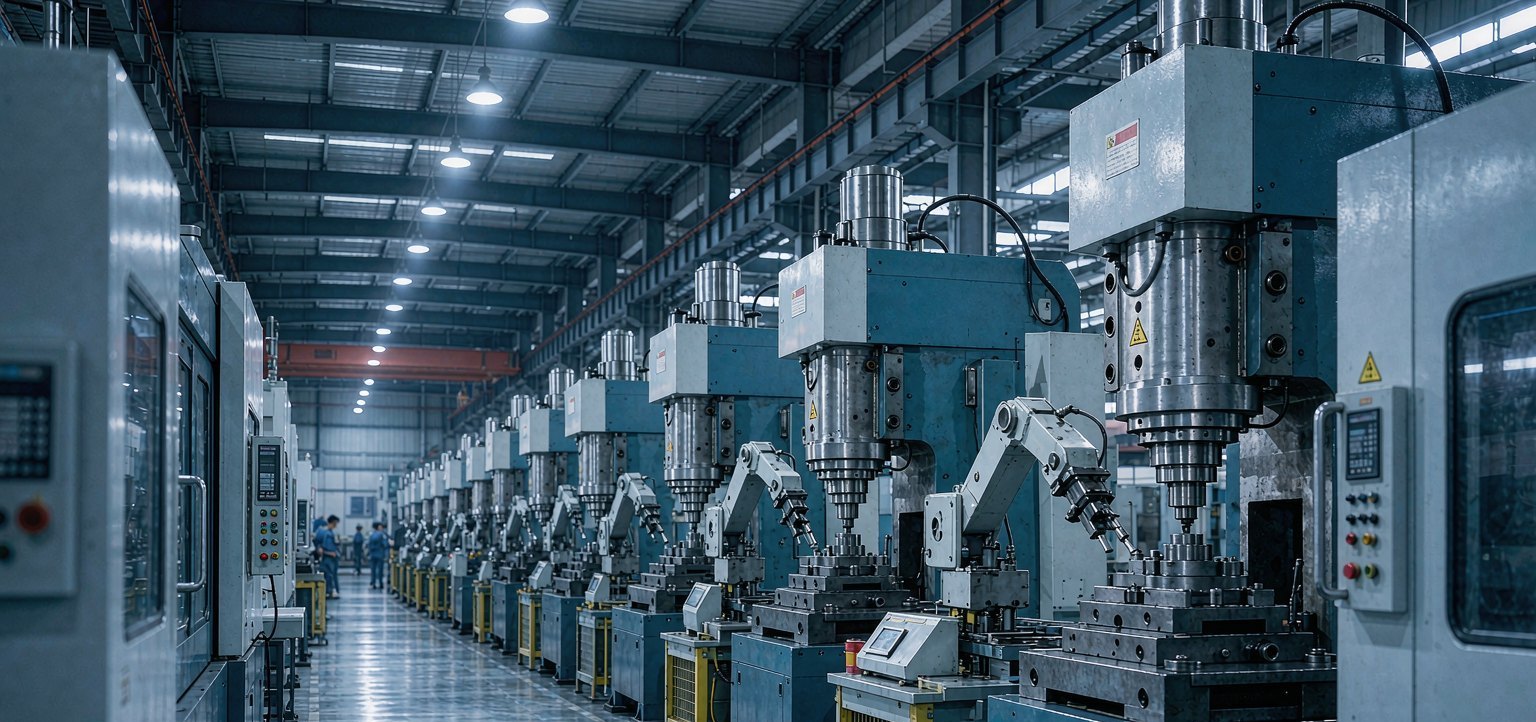
Cold forging hall
Two-, three- and four-station headers run from 0.8 to 6.0 mm wire. The hall is arranged by size band so that micro work is not interrupted by larger runs — at M1, a changeover is a precision event, not a quick setup.
M0.5 – M6 · up to 400 pcs/min
03 / 09
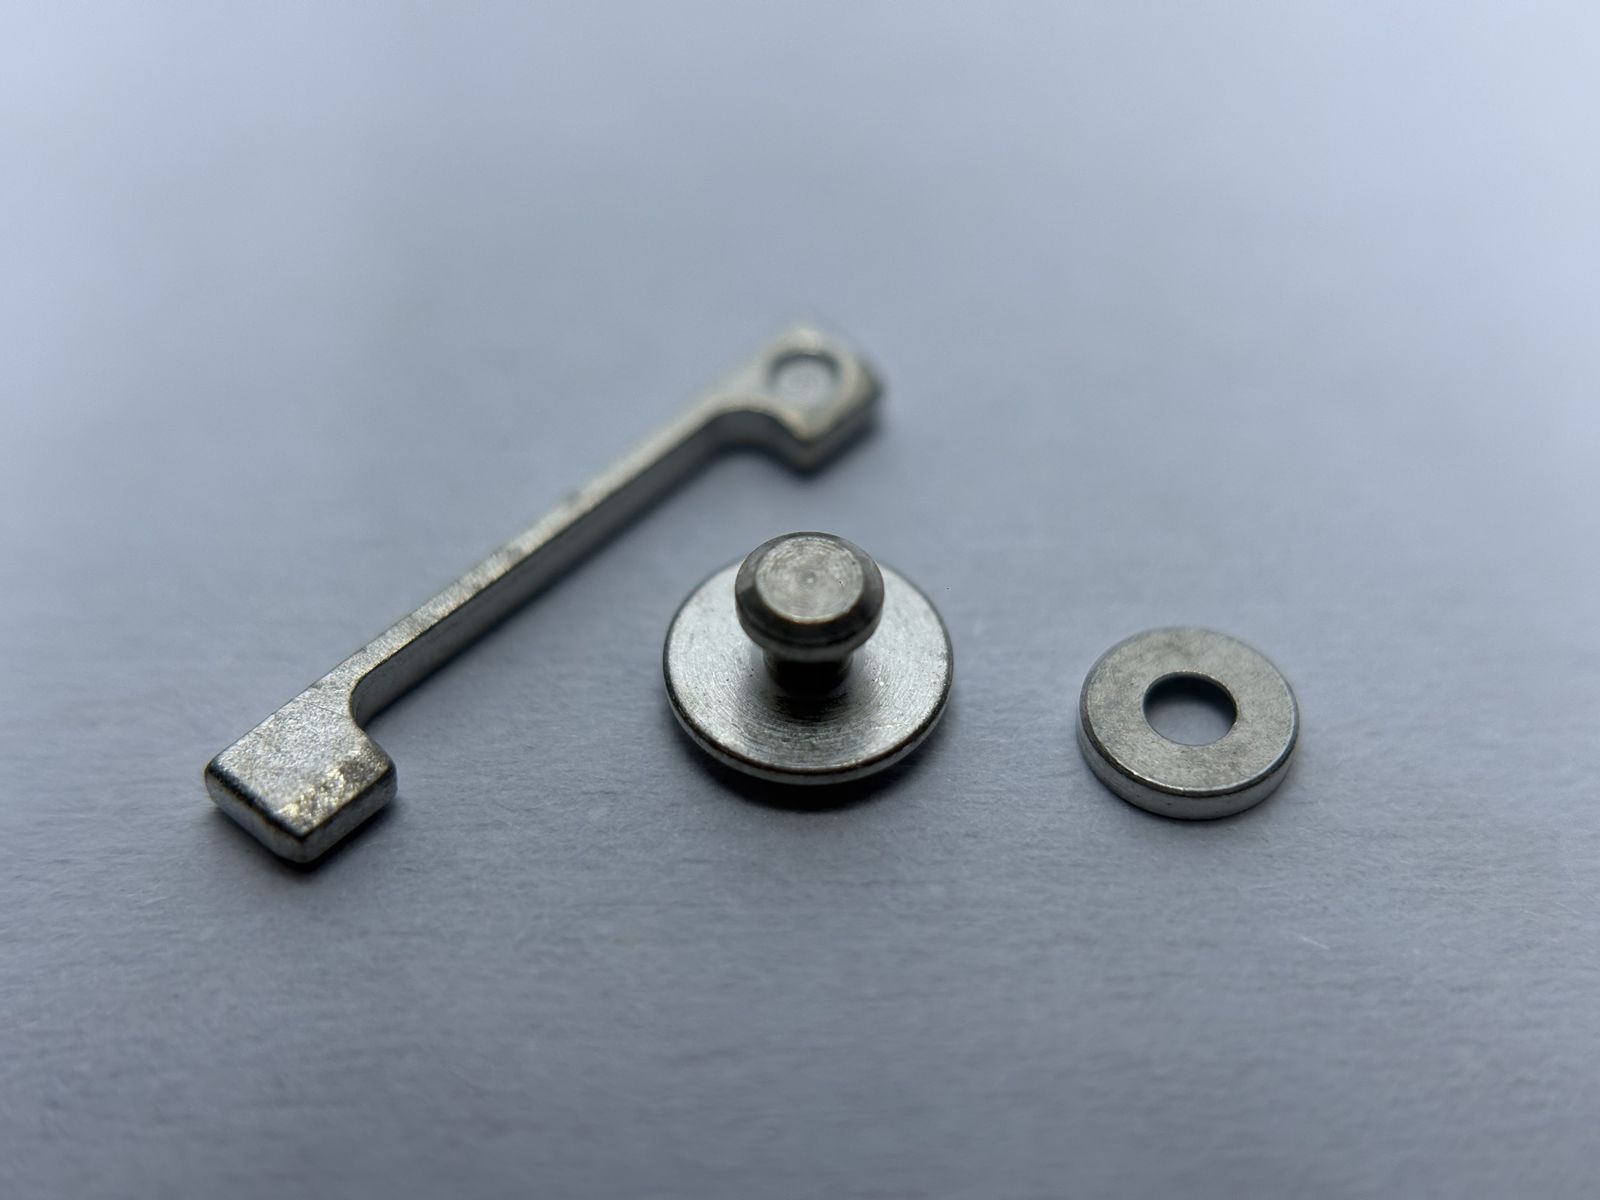
Die shop
Wire EDM, jig grinding and optical profile grinding sit beside the presses. A punch can be dressed, measured and back in the machine within a shift, which is what makes a 7–12 day new-die lead time realistic.
In-house die design, build and maintenance
04 / 09
Heat treatment
Controlled atmosphere furnaces with carbon potential monitoring, oil and polymer quench, and tempering ovens. Each load carries a temperature and atmosphere chart; hardness and case depth are verified on a sample.
Carburising · quench and temper · stress relief
05 / 09
Plating and PVD
Barrel zinc, zinc-nickel and nickel lines, plus multi-arc and magnetron sputtering chambers for TiN, CrN, TiCN and DLC. Coating thickness is measured at the head, shank and thread root.
96 – 720 h salt spray · PVD 2 – 5 µm
06 / 09
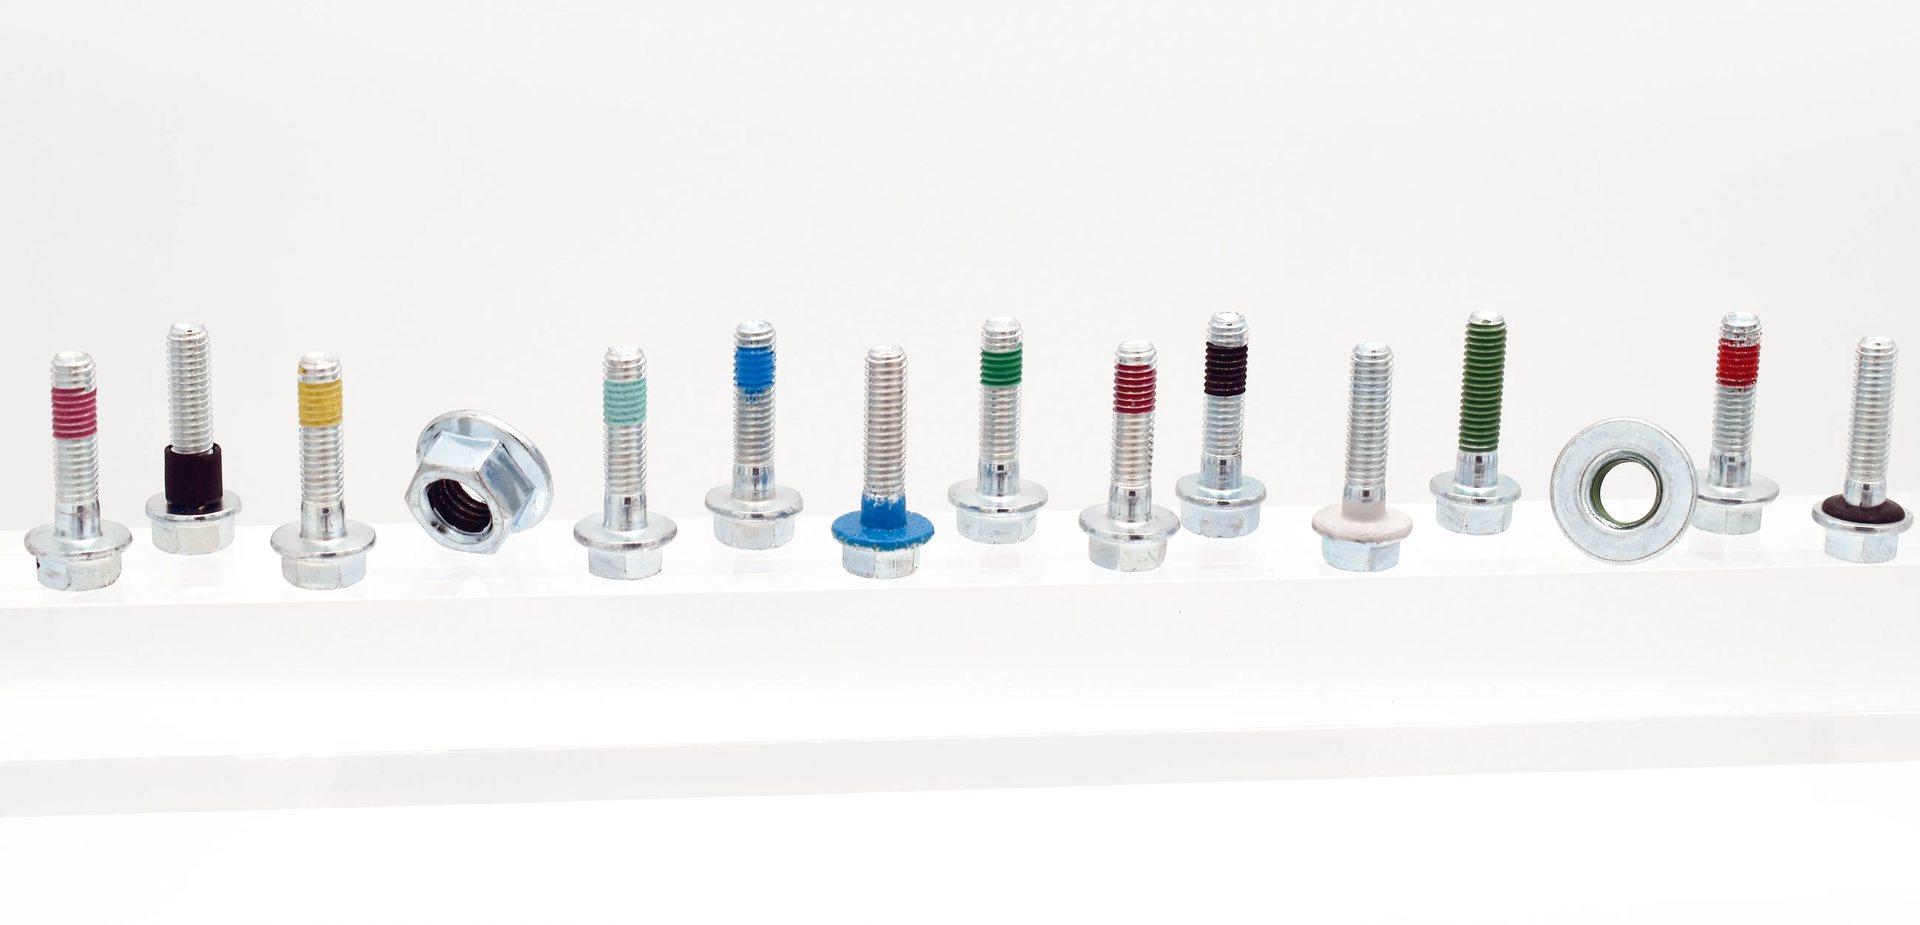
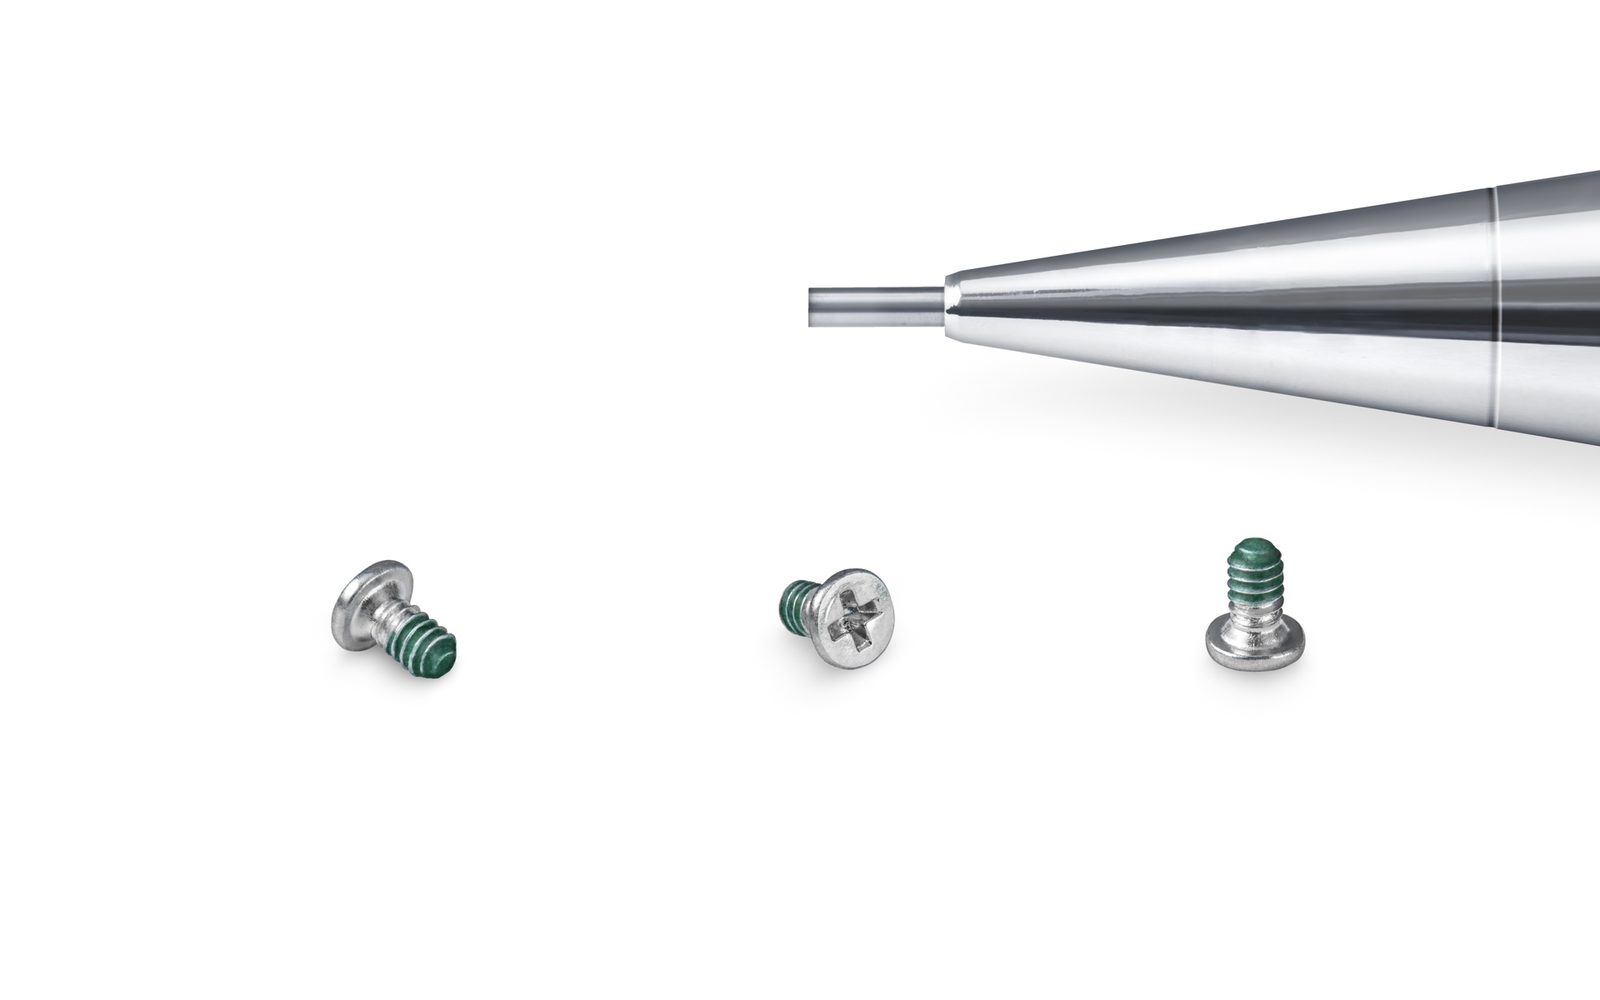
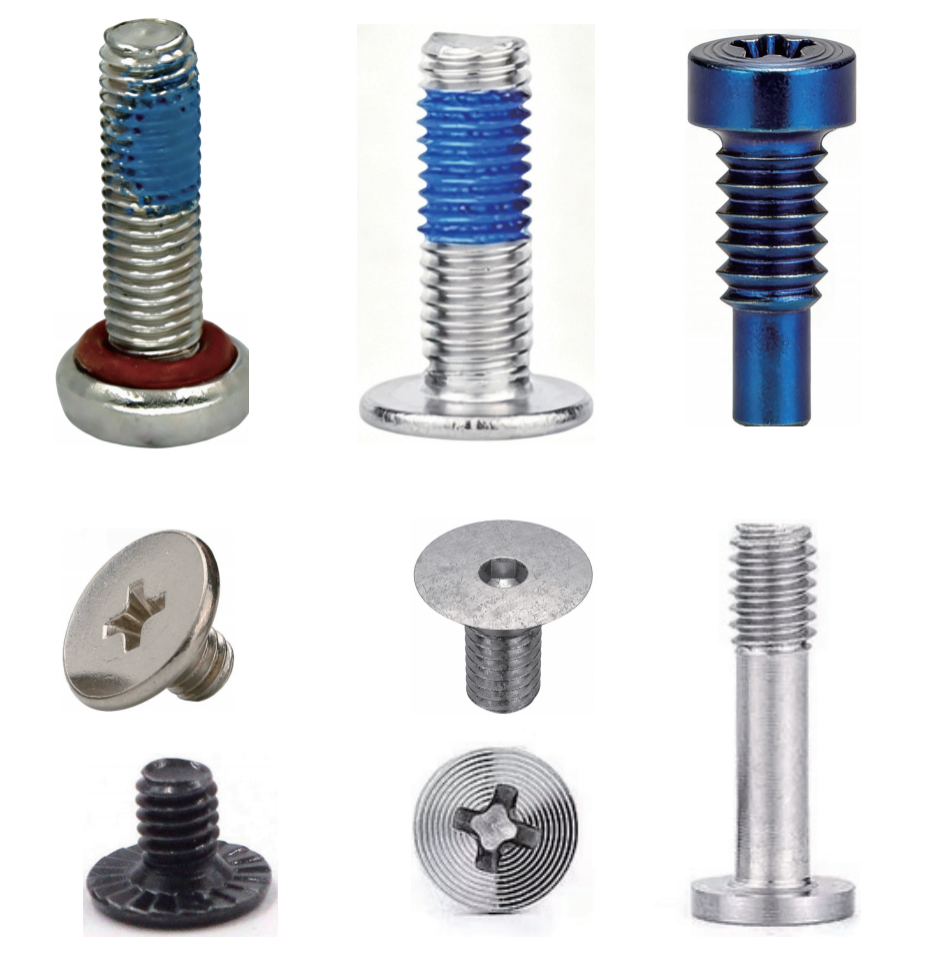
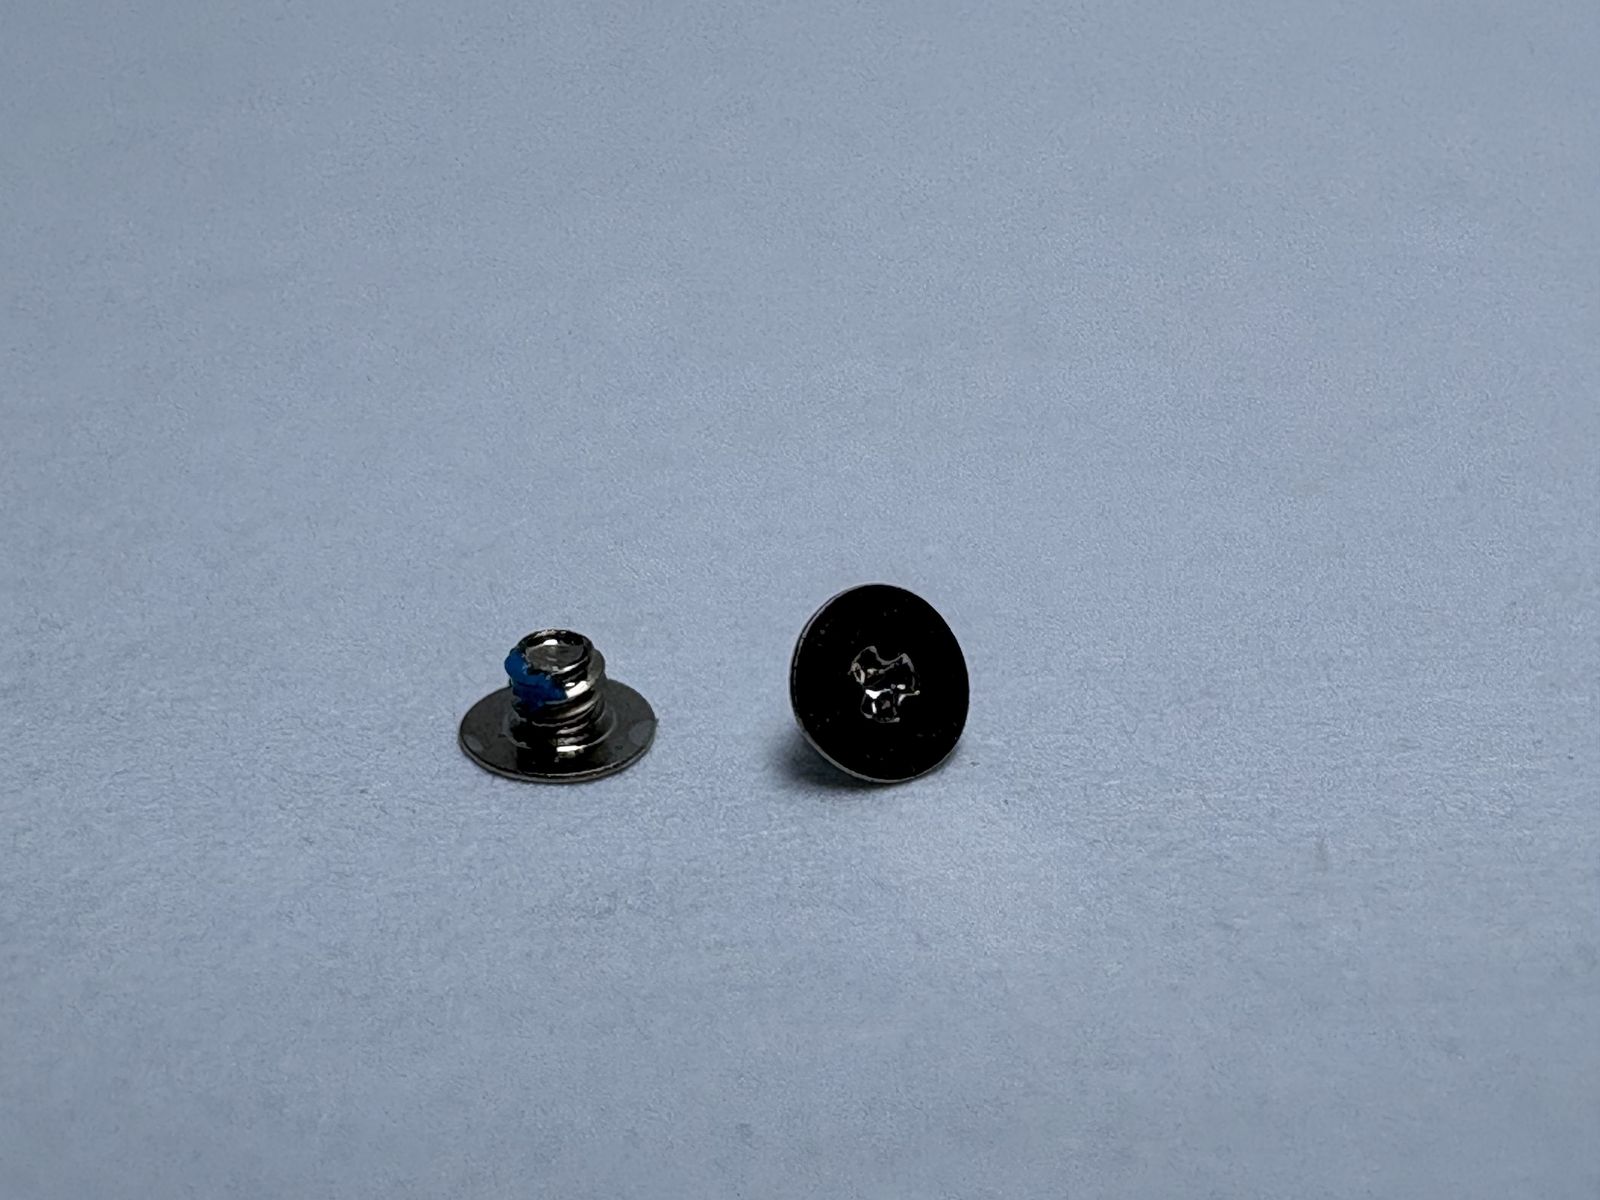
Precoating cell
Nylon powder, micro-encapsulated adhesive and 3M tape are applied at a controlled position on the thread. Position and mass are verified optically; torque is tested on a sample from each batch.
Patch position and mass controlled
07 / 09
Optical sorting
Vision and laser inspection at up to 2,000 pieces per minute. Rejects are counted and reconciled against the input quantity, so a mixed or incomplete lot cannot leave the building.
100% of production lots sorted
08 / 09
Quality laboratory
Vision metrology, optical comparator, micro-hardness, torque and tensile testing, salt spray and XRF. The lab is next to the sorting area so that a drift can be investigated without stopping the line.
0.001 mm resolution · ASTM B117
09 / 09
Packing and dispatch
Reel, matrix tray, bulk bag or cleanroom bag, labelled with lot code, quantity, size, finish and inspection status. Cartons are palletised for freight or consolidated for courier.
EIA-481 reels · cleanroom packing available
Before you visit
What we will show you
A visit can be general or focused. Tell us what you need to see and we will build the route around it.
Process walk-through
The full route from wire to carton, with the control point at each stage.
Your part on the line
If we already make your part, we will schedule the run during your visit.
Laboratory demonstration
Hardness, torque, salt spray and vision measurement, run on a sample.
Quality system review
Control plans, PFMEA, lot records and the CAPA process.
Arrange a plant visit
Bekasi is about an hour from Jakarta by toll road. Send your preferred dates and the focus of the visit, and we will confirm the production schedule.