Capabilities
From wire rod to packed carton, under one roof
Six process areas, one plant, one traceability chain. A lot never leaves our control between forging and packing — which is why a dimensional or finish drift is caught before it reaches your line.
Process areas
Six capabilities that decide the part
Each of these can be bought separately from different suppliers. Keeping them together is what makes a tolerance achievable rather than a negotiation.
Capability
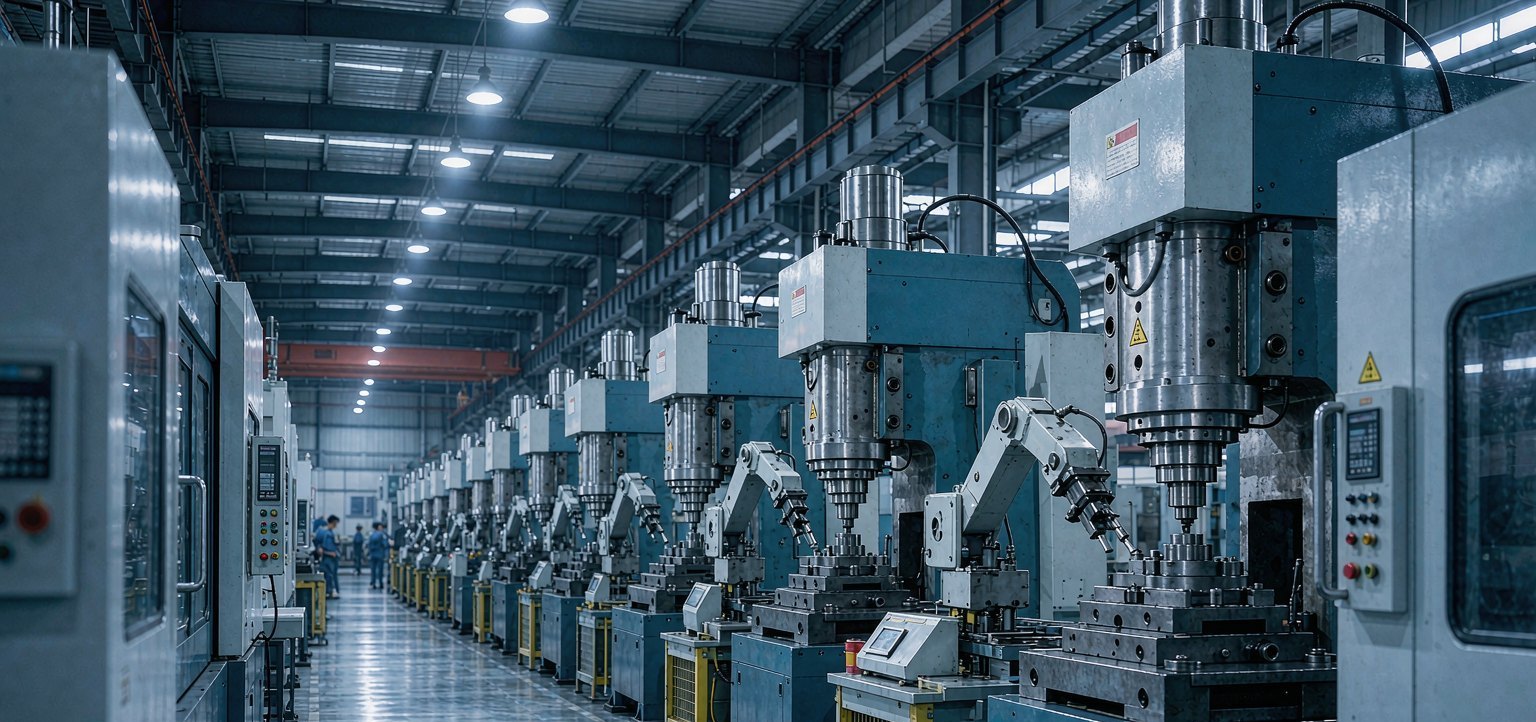
Cold Forging
Two-, three- and four-station cold heading machines form micro screw blanks from wire without cutting, preserving grain flow through the head and shank.
Capability
Heat Treatment
Controlled atmosphere heat treatment for case depth, core hardness and hydrogen embrittlement relief — with batch records for every lot.
Capability
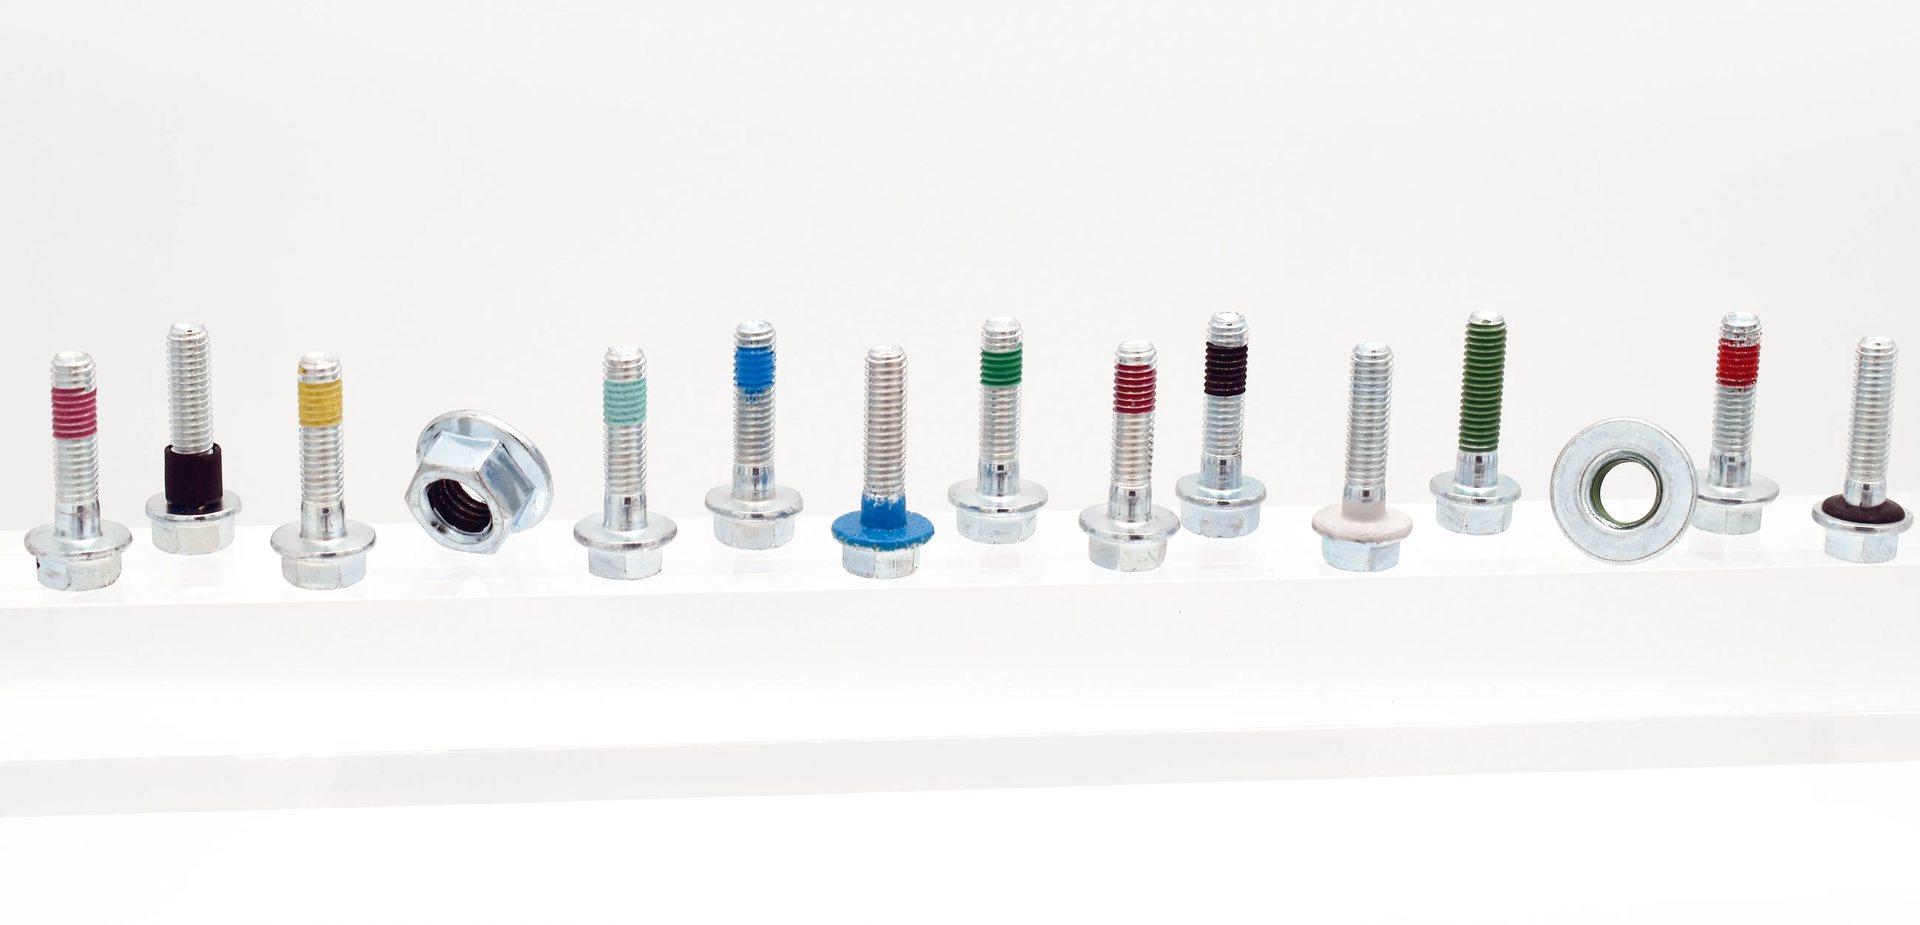
Surface Finishing
Barrel plating, passivation and PVD coating lines for corrosion resistance, conductivity and cosmetic appearance — with coating thickness verified at the thread root.
Capability
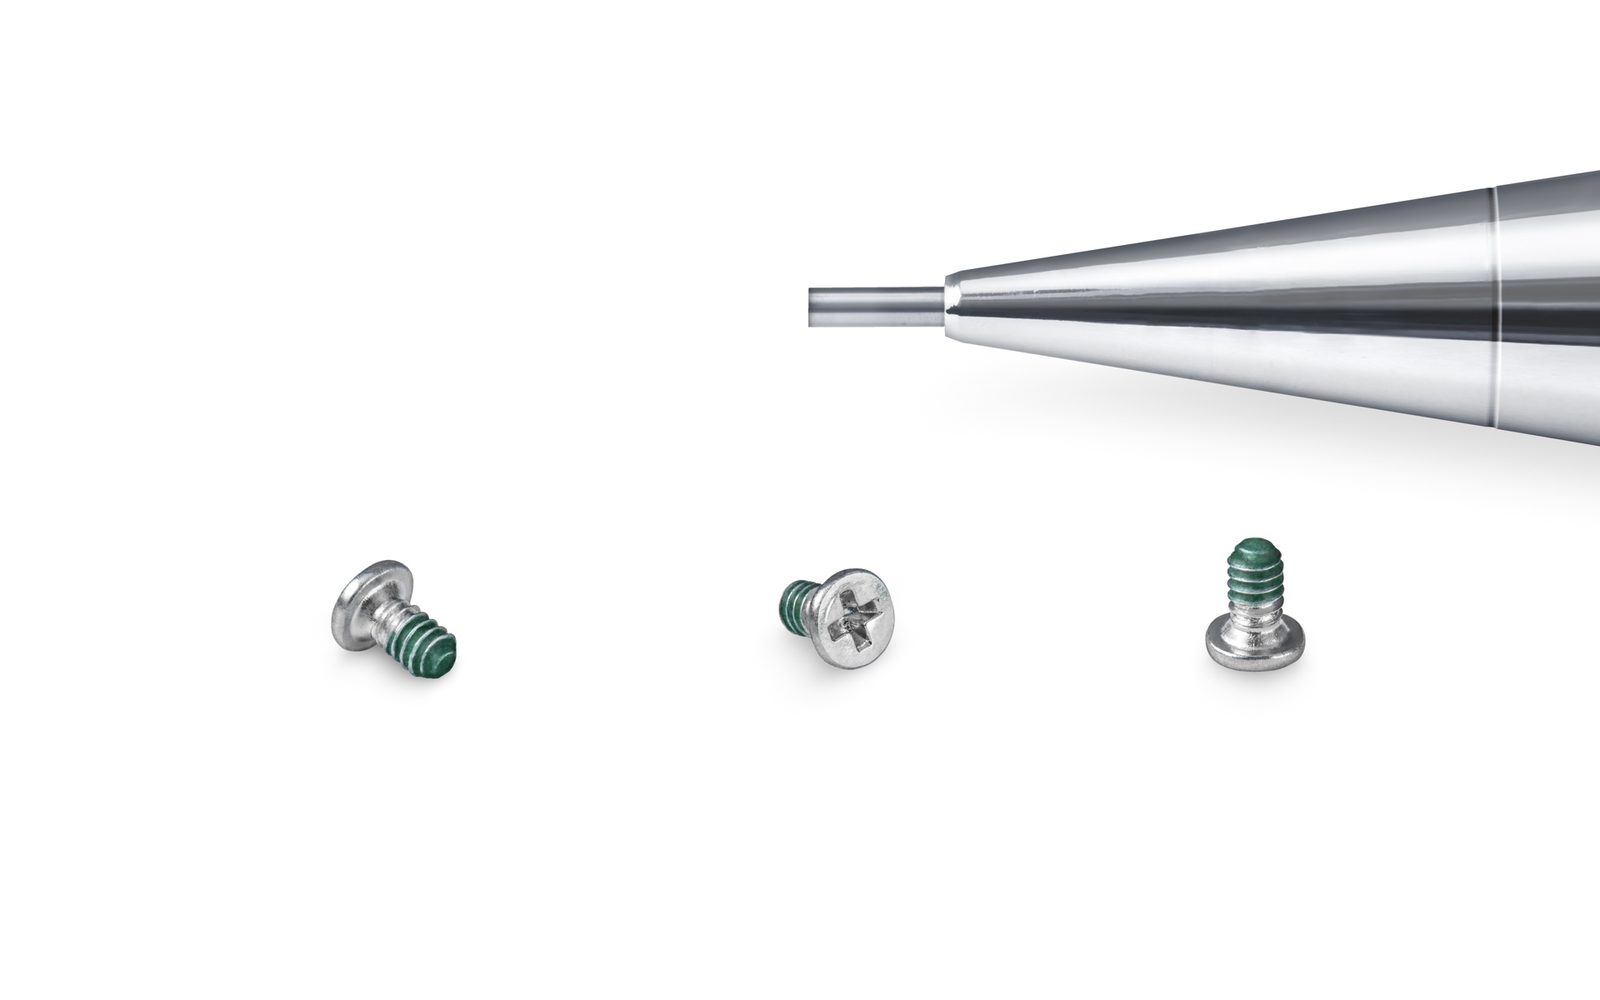
Precoating & Patch
Automated application of locking and sealing elements at a controlled thread position, with break-loose torque verified per batch.
Capability
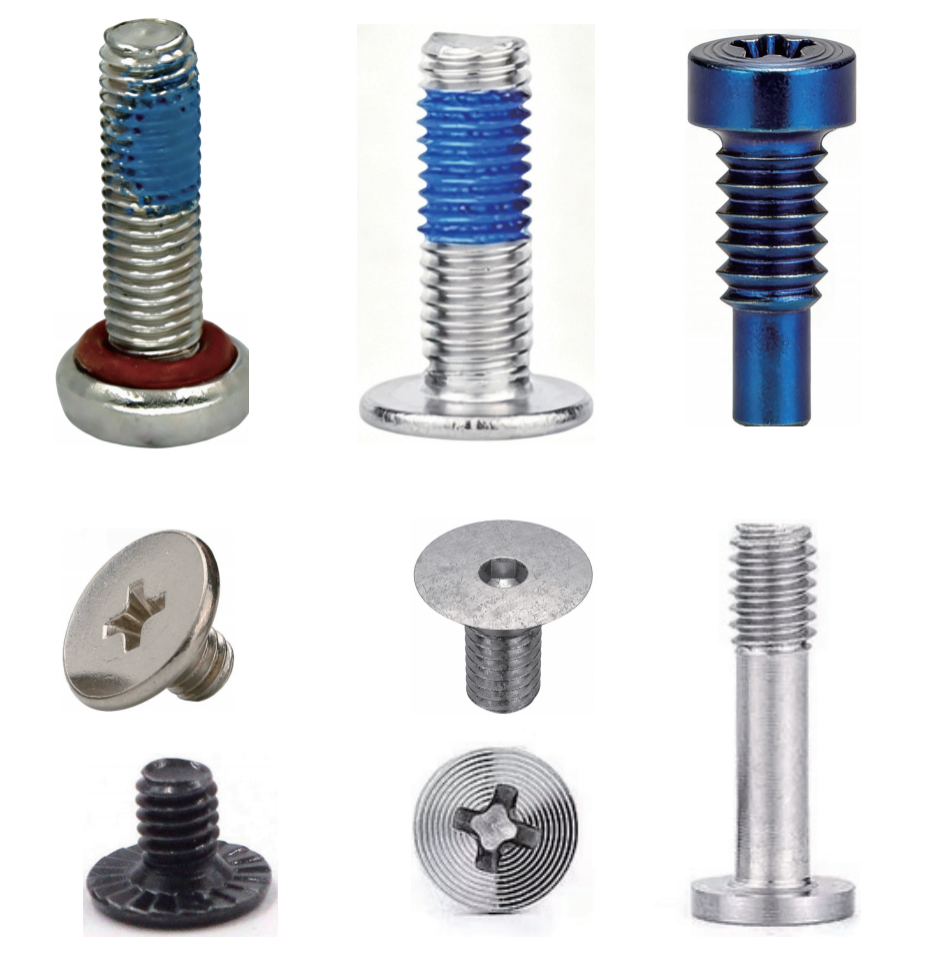
Quality Laboratory
An in-house laboratory covering dimensional metrology, hardness, torque, salt spray and material verification — so results are not outsourced and delayed.
Capability
Optical Sorting & Packaging
Vision-based sorting removes bent, short, mixed and defective parts before packing, with reel, tray and cleanroom bag options.
End-to-end flow
The route a part takes
Eight steps from incoming wire to a labelled carton. Every step produces a record linked to the lot code.
Wire intake
Certified wire, checked for diameter, ovality and hardness, linked to a heat number.
Cold forging
2–4 station heading of head, shank and point from 0.8–6.0 mm wire.
Thread rolling
Class 6g / 6f threads rolled with flat or cylindrical dies.
Heat treatment
Carburising or quench-and-temper with recorded atmosphere and hardness.
Coating
Zinc, zinc-nickel, nickel, passivation or PVD, thickness checked at the thread root.
Precoating
Nylon patch or encapsulated adhesive at a controlled position on the thread.
Optical sorting
Vision plus laser inspection at up to 2,000 pcs/min, with reject reconciliation.
Packing
Reel, tray, bulk or cleanroom bag, labelled and lot-traced.
Equipment
Plant equipment and capability
Representative equipment list. Capacity depends on size, geometry and finish — ask for a specific part and we will confirm the route.
| Area | Equipment | Capability |
|---|---|---|
| Forging | Two- to four-station headers | M0.5 – M6, up to 400 pcs/min |
| Tooling | Wire EDM, jig grinder, optical profile grinder | In-house die design and maintenance |
| Threading | Flat-die and cylindrical rollers | Class 6g / 6f, M0.5 – M6 |
| Heat treatment | Controlled atmosphere furnaces, oil and polymer quench | Case depth 0.05 – 0.25 mm |
| Plating | Barrel zinc, zinc-nickel and nickel lines | 5 – 15 µm, 96 – 720 h salt spray |
| PVD | Multi-arc and magnetron sputtering chambers | TiN, CrN, TiCN, TiAlN, DLC, 2 – 5 µm |
| Precoating | Nylon patch cell, encapsulant dispenser, tape applicator | Position and mass controlled |
| Inspection | Vision, optical comparator, micro-hardness, salt spray, XRF | 0.001 mm dimensional resolution |
| Sorting | Vision plus laser sorting machines | Up to 2,000 pcs/min |
| Packing | Reel taper, matrix tray, cleanroom bag sealer | EIA-481, Class 100,000 area |
Quality system
Certified, audited, documented
Certification establishes the system. The lot record is what proves it was followed on the day your parts were made.
ISO 9001:2015
Quality management system
IATF 16949:2016
Automotive quality management
ISO 14001:2015
Environmental management
ISO 45001:2018
Occupational health & safety
IECQ QC 080000
Hazardous substance process
RoHS / REACH
Substance compliance
Dimensional metrology
Vision systems, optical comparator, air gauges and micrometers with 0.001 mm resolution.
Mechanical testing
Micro-hardness, case depth, torque-to-preload, tensile and pull-out testing.
Corrosion and material
ASTM B117 salt spray to 1,000 h, XRF coating thickness, metallography.
Why one site matters
Every handoff is a place where tolerance is lost
When forging, heat treatment and coating happen at three different companies, each handoff adds handling damage, a new incoming inspection and a new opportunity for an undocumented process change. Keeping them together removes those handoffs.
It also makes problem-solving faster. If a plating batch shows poor adhesion, the forging and heat treatment records are in the same building, so the cause can be traced the same day rather than through three supplier quality departments.
1
Plant, one traceability chain
6
Process areas in-house
Forging hall · Cikarang Utara Ask us to route your part
Send a drawing and an annual volume. We will reply with the process route, the tolerance we can hold and the lead time — before any commercial discussion.