Capability
Optical Sorting & Packaging
100% optical sorting and application-specific packing
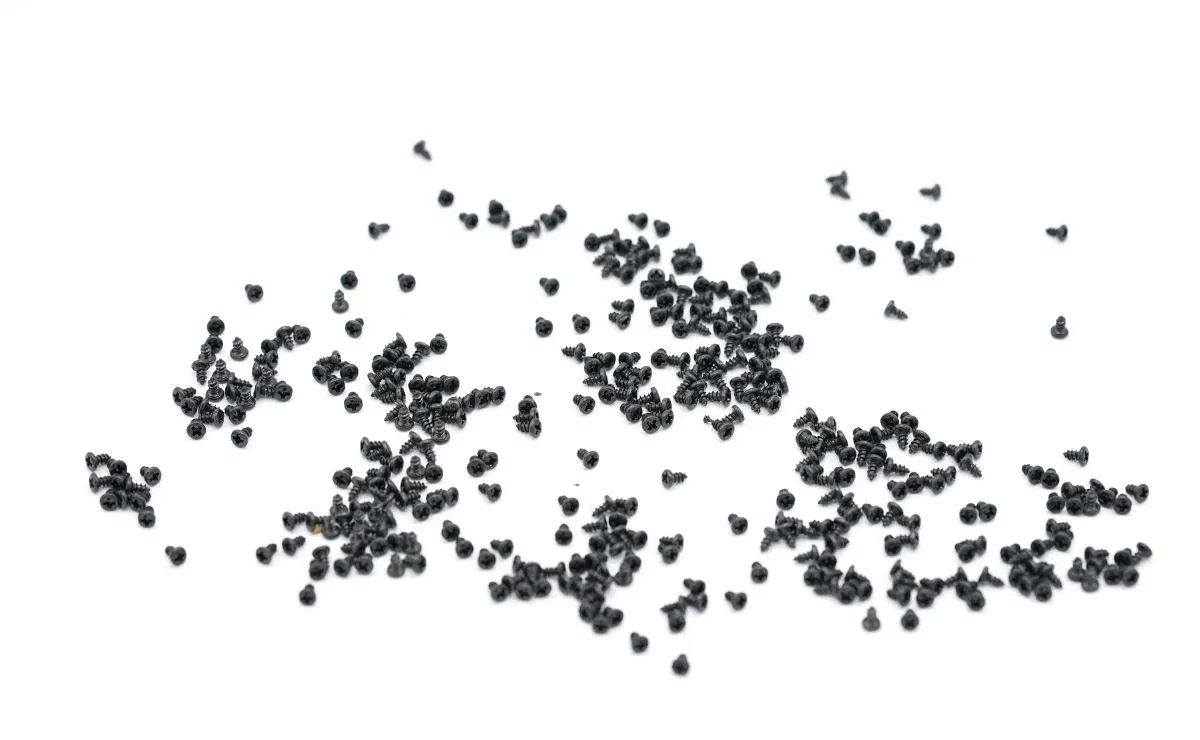 Optical Sorting & Packaging · Bekasi plant
Process overview
100% optical sorting and application-specific packing
At M1.0 a defective screw is almost invisible. A bent shank, a short length or a missing thread may pass a visual check but will jam a feeder or cross-thread a housing. The cost of that failure is not the screw — it is the stopped line, the rework and the containment report.
Every production lot passes through optical sorting that combines vision for head geometry, drive presence and surface defects with laser measurement for length and diameter. Parts outside the window are ejected, and the accepted stream is packed according to the customer’s feeding method: taped reel, matrix tray, bulk bag or cleanroom bag.
Step by step
How the process runs
Each step has a defined control point. The sequence is not arbitrary — changing it changes the result.
De-burring and cleaning
Parts are tumbled and degreased so that debris does not create false rejects during inspection.
Vision inspection
Cameras check head diameter, head height, drive presence, concentricity and surface defects at up to 2,000 pcs/min.
Laser dimensional check
Laser gauges measure length and shank diameter, rejecting parts outside the drawing window.
Ejection and verification
Rejected parts are ejected into a locked bin, counted and reconciled against the input quantity.
Packing
Accepted parts are packed on taped reel, in matrix trays, or in bulk and cleanroom bags according to the assembly method.
Label and traceability
Each package carries lot code, quantity, size, finish and inspection status, linked to the production record.
Specification
Process window and capability
The numbers below define what the process can hold repeatably. They are not laboratory bests.
Sorting rate
Up to 2,000 pcs/min
Vision checks
Head Ø, head height, drive presence, concentricity, surface
Laser checks
Length, shank diameter
Reject reconciliation
Input vs accepted vs rejected, per lot
Reel standard
EIA-481, 8 – 44 mm tape
Tray options
Anti-static matrix tray, custom cavity
Bag options
Bulk, cleanroom, moisture barrier
Counting accuracy
±0.1% by weight, verified by piece count
Label content
Lot, quantity, size, finish, date, QR
Packing area
Class 100,000 cleanroom available
Equipment
What the line is built on
Capacity figures are per machine and assume a standard part. Complex geometry reduces throughput.
| Equipment | Specification |
|---|---|
| Optical sorting machines | Vision + laser, up to 2,000 pcs/min |
| Reel taping | 8 – 44 mm tape width, EIA-481 compatible |
| Matrix tray | Anti-static, custom cavity |
| Cleanroom bag sealer | Class 100,000 packing area |
| Counting and weighing | 0.001 g resolution, piece-count verification |
| Label system | Lot code, QR, customer part number |
Process control
What is checked, and when
A control that is not recorded is not a control. Each item below generates a record linked to the lot code, retained for the programme duration.
01
Sorter calibration and master sample verification at start of shift
02
Reject bin reconciliation per lot
03
Piece-count verification by weight and sampling
04
Label accuracy check before carton sealing
05
Cleanroom particle monitoring where applicable
06
Packaging integrity and desiccant check
07
Retained sample per lot
08
Traceability from lot code to production record
Questions
Sorting & Packing FAQ
Practical questions from sourcing and engineering teams.
Is sorting really 100%?
Can you pack on reel for our feeder?
Do you offer cleanroom packing?
How do you prevent mixed sizes in a carton?
Related capabilities
What happens before and after
These processes are usually sequenced with the one above.
Capability
Quality Laboratory
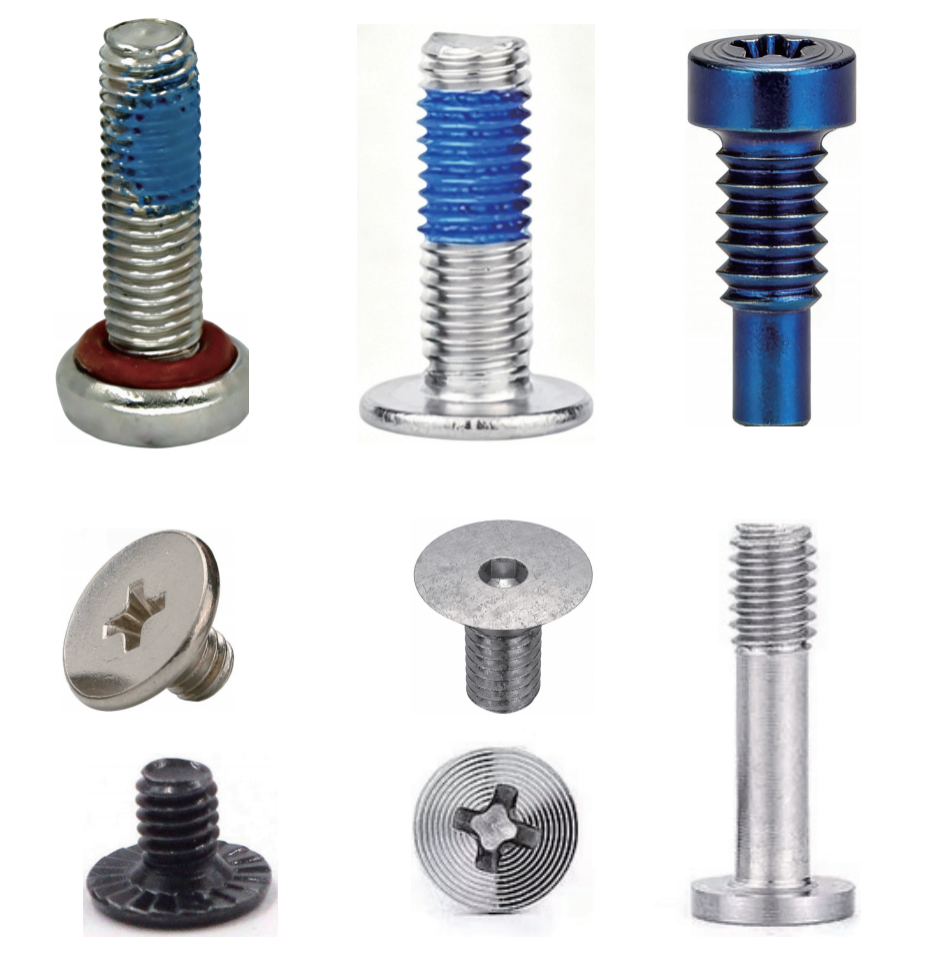
An in-house laboratory covering dimensional metrology, hardness, torque, salt spray and material verification — so results are not outsourced and delayed.
Capability
Precoating & Patch
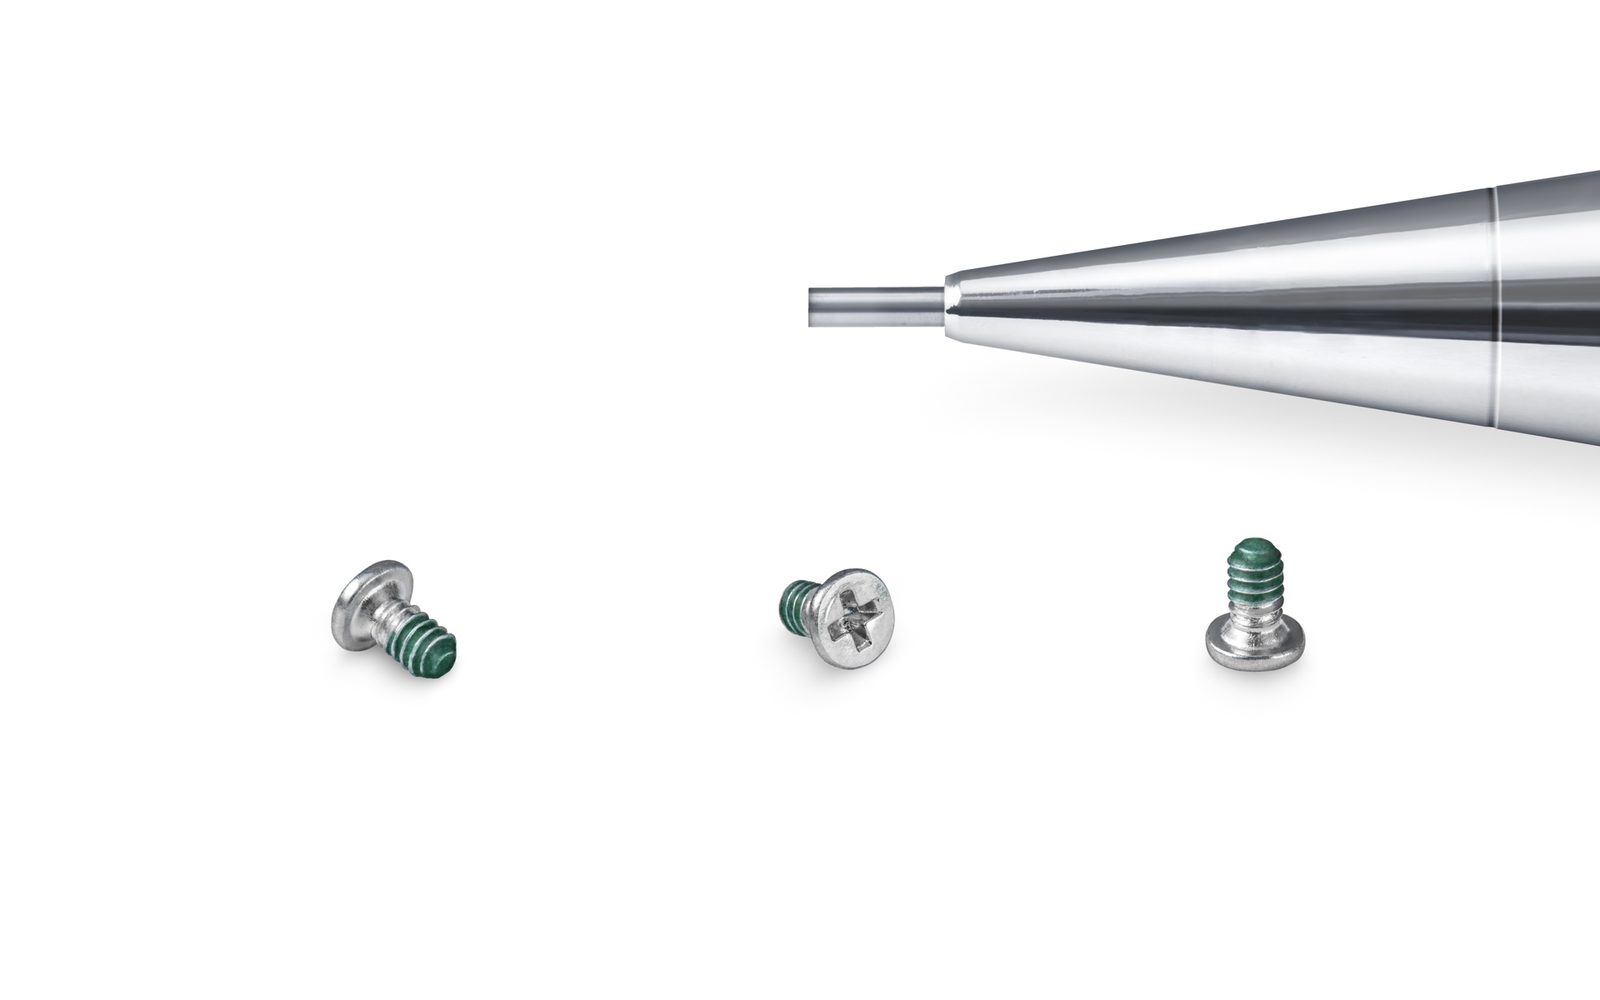
Automated application of locking and sealing elements at a controlled thread position, with break-loose torque verified per batch.
Capability
Surface Finishing
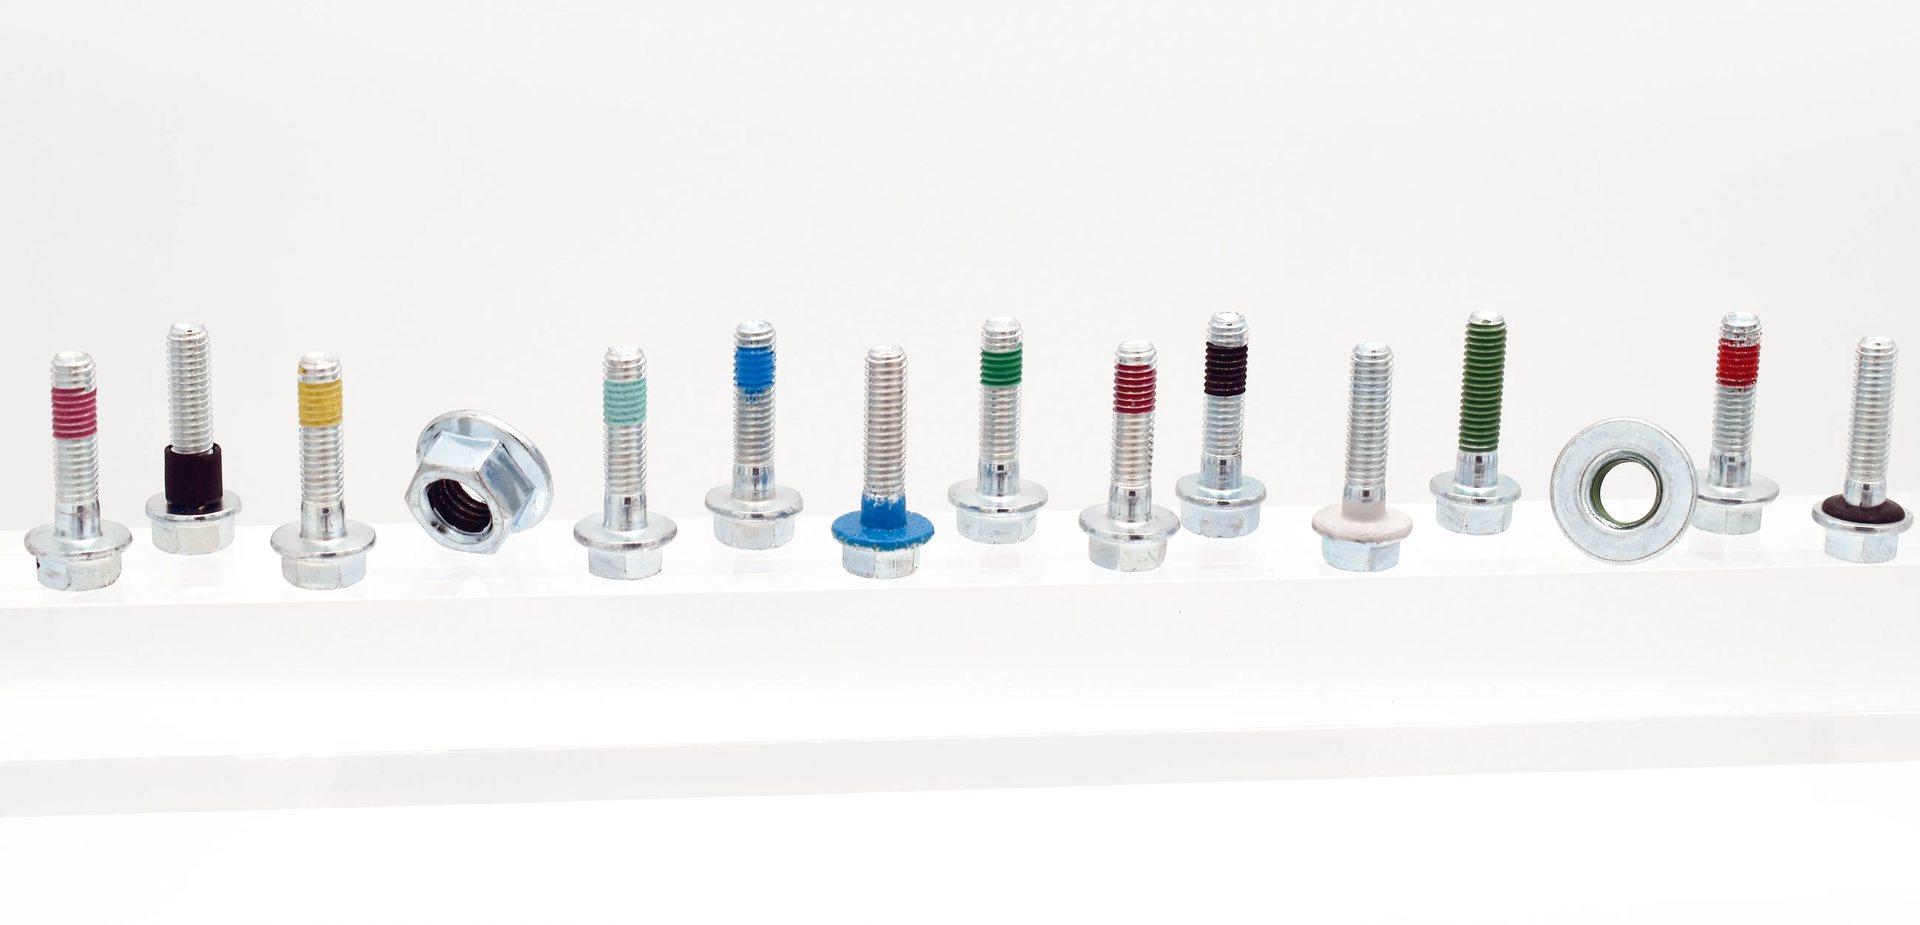
Barrel plating, passivation and PVD coating lines for corrosion resistance, conductivity and cosmetic appearance — with coating thickness verified at the thread root.
Capability
Cold Forging
Two-, three- and four-station cold heading machines form micro screw blanks from wire without cutting, preserving grain flow through the head and shank.
Need sorting & packing for your part?
Send the drawing and the annual volume. We will confirm feasibility, tolerance and lead time in the quotation.