Boss Design for Thread-Forming Screws in Plastic: The Rules That Prevent Cracks
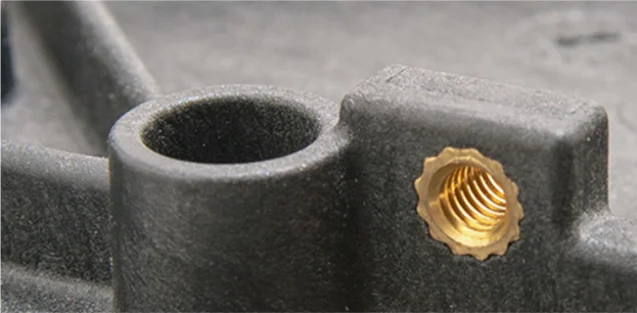
A thread-forming screw into plastic is a self-tapping system where the boss is half the fastener. Getting boss geometry right eliminates the classic failures: cracks at assembly, creaking joints, lost clamp after weeks.
The diameter ratios
For glass-filled thermoplastics, pilot-hole diameter runs 80–85% of screw nominal; unfilled materials take 70–80%. Boss OD should be 2–2.5× the pilot diameter — too thin and the boss cracks from hoop stress; too thick and sink marks appear on the cosmetic face. Depth: engagement of 2–2.5× nominal diameter, with relief at the bottom for displaced material.
Details that separate good from fragile
- Radius at the boss root fillet: sharp corners initiate cracks under clamp load.
- Drive torque must exceed strip torque margin properly — spec forming torque strip ratio ≥ 2:1 for line robustness.
- Moisture changes nylon dimensions: validate at 50% RH conditioning, not dry-as-molded.
Test like production
Assemble 30 joints at line torque, then thermal-cycle and re-measure residual clamp. Topprecision manufactures thread-forming screws with plastic-specific thread geometry (asymmetric flanks, reduced drive torque) and co-reviews boss drawings with customers' molding engineers — the fastest route to a silent joint.