Cold Heading vs Machining: How the Process Decides the Fastener's Strength
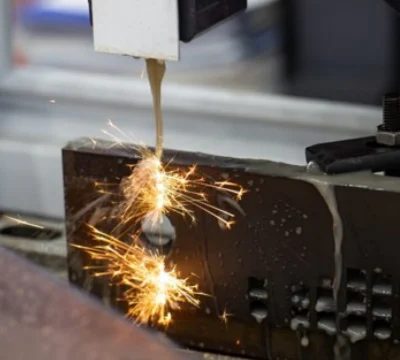
Two screws from identical steel can differ 30% in fatigue life. The difference is not chemistry — it is grain flow.
What cold heading does to the metal
Cold heading deforms wire at room temperature between dies. The crystal grains elongate and flow around the head contour continuously — like wood grain around a knot. Cut threads then roll the shank, densifying surface layers. The result: continuous grain lines following the part geometry, work-hardened surfaces, and fatigue strength a machined-from-bar equivalent cannot match.
Where machining remains right
- Low volumes, prototypes, and diameters beyond heading machine capability.
- Complex heads (custom hexalobes, flange-under-cut geometries) where die cost is unjustified.
- Ultra-precise micro parts where machining centers hold tighter tolerances.
The economic crossover
Above roughly ten thousand pieces, heading die amortization beats per-part machining cost — usually by a factor of five on simple geometries. Topprecision runs both processes and quotes honestly: we recommend heading where volume justifies it and machining where flexibility does, and our cold-headed 7-series aluminum bolt line exists precisely because grain flow makes aluminum bolts structurally viable.