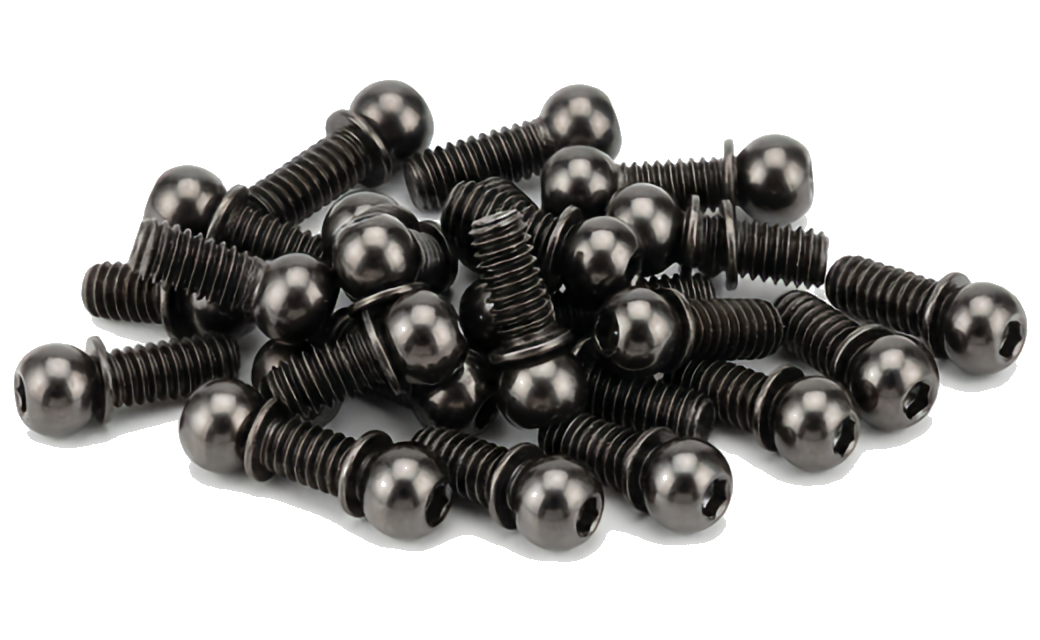
PECVD-DLC (Plasma-Enhanced CVD Diamond-Like Carbon)
PECVD-DLC coating: a low-temperature DLC process for heat-sensitive parts, with 200-500 h protection and low friction.
| Finish Code | TZ018 |
|---|---|
| Environmental Grade | Low-temperature vacuum deposition; clean and pollution-free. RoHS compliant |
| Salt Spray Standard | 200-500 h; strongly dependent on substrate pre-treatment |
| Appearance / Colour | Dark grey to black |
| Suitable For | Low-temperature precision fasteners, optical components, low-friction micro screws |
| Features | Low processing temperature; low friction; wear resistant |
| Environmental Compliance | REACH and RoHS compliant |
Overview
Surface finishing on a fastener is a functional coating, not a cosmetic one: it sets the friction coefficient that determines how much of the applied torque becomes clamp load, and it defines how long the part survives in a corrosive environment. Two finishes that look identical can differ by a factor of several in salt-spray hours and by enough in friction to change the torque specification. This listing: finish code TZ018, salt spray 200-500 h, appearance / colour Dark grey to black, environmental compliance REACH and RoHS compliant.
What sets this listing apart: Environmental Grade Low-temperature vacuum deposition; Features Low processing temperature.
Advantages
Friction coefficient changes with coating: a zinc-flake coating typically runs lower and more consistently than electroplated zinc, which is why torque tables are finish-specific.
Barrier coatings protect the base metal, while sacrificial coatings protect the steel even at a scratch; the choice depends on whether the joint will be damaged in service.
Hydrogen embrittlement risk separates processes: electroplating on high-strength steel needs a de-embrittlement bake, while mechanical and flake coatings avoid the risk entirely.
Applications
Automotive underhood and body joints, outdoor equipment, marine and coastal installations, electronics hardware, and any joint where the torque specification is tied to a friction value.
Quote the standard, the hours and the acceptance criterion together — a salt-spray figure without the test method is not a specification. Check that the coating process is compatible with the core hardness of the part.
Product information is supplied by Toprecision. Custom parts can be produced to drawing — contact us for samples or a quotation.
Specifications across this series
2 parts in this series
| Part | Finish Code | Environmental Gr… | Salt Spray Stand… | Appearance / Col… |
|---|---|---|---|---|
| PECVD-DLC (PECVD CVD DLC) · TZ018 / Low-temperature vacuum deposition; clean and pollution-free. RoHS compliant / 200-500 h; strongly dependent on substrate pre-treatment | TZ018 | Low-temperature vacuum deposition; clean and pollution-free. RoHS compliant | 200-500 h; strongly dependent on substrate pre-treatment | Dark grey to black |
| CVD Hard Coating · TZ303 / REACH / RoHS compliant / Not applicable (functional coating) | TZ303 | REACH / RoHS compliant | Not applicable (functional coating) | Grey to black, matt |
Values are taken from each part’s own attribute set. Changing length, material or finish changes pull-out strength and installation torque, so compare the row that matches your drawing.
Selection and test data: engagement length, standards, salt-spray hours
FAQ
What does this finish provide?
Finish Code TZ018, Environmental Grade Low-temperature vacuum deposition, Salt Spray Standard 200-500 h, Appearance / Colour Dark grey to black.
How does it affect torque and friction?
Carbon Steel.
What should I verify before ordering or installing it?
Quote the standard, the hours and the acceptance criterion together — a salt-spray figure without the test method is not a specification. Check that the coating process is compatible with the core hardness of the part.