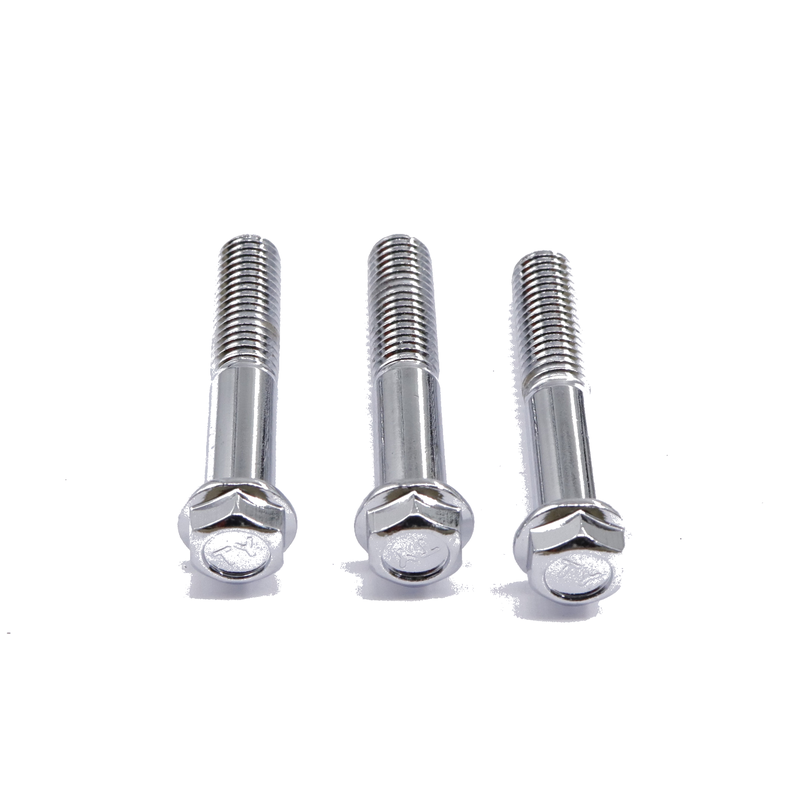
Chrome Plating (Bright Chrome)
Bright chrome plating: a decorative mirror finish with 48-120 h protection, improving as the underlying nickel layer is thickened.
| Finish Code | TZ013 |
|---|---|
| Environmental Grade | Trivalent chromium decorative plating, RoHS compliant |
| Salt Spray Standard | 48-120 h; increases with nickel layer thickness |
| Appearance / Colour | Mirror-bright chrome |
| Suitable For | Exposed decorative screws; precision fasteners with high appearance requirements |
| Features | Decorative; wear resistant; tarnish resistant |
| Environmental Compliance | REACH and RoHS compliant |
Overview
Surface finishing on a fastener is a functional coating, not a cosmetic one: it sets the friction coefficient that determines how much of the applied torque becomes clamp load, and it defines how long the part survives in a corrosive environment. Two finishes that look identical can differ by a factor of several in salt-spray hours and by enough in friction to change the torque specification. This listing: finish code TZ013, salt spray 48-120 h, appearance / colour Mirror-bright chrome, environmental compliance REACH and RoHS compliant.
What sets this listing apart: Features Decorative; Salt Spray Standard 48-120 h.
Advantages
Barrier coatings protect the base metal, while sacrificial coatings protect the steel even at a scratch; the choice depends on whether the joint will be damaged in service.
Hydrogen embrittlement risk separates processes: electroplating on high-strength steel needs a de-embrittlement bake, while mechanical and flake coatings avoid the risk entirely.
Friction coefficient changes with coating: a zinc-flake coating typically runs lower and more consistently than electroplated zinc, which is why torque tables are finish-specific.
Applications
Automotive underhood and body joints, outdoor equipment, marine and coastal installations, electronics hardware, and any joint where the torque specification is tied to a friction value.
Quote the standard, the hours and the acceptance criterion together — a salt-spray figure without the test method is not a specification. Check that the coating process is compatible with the core hardness of the part.
Product information is supplied by Toprecision. Custom parts can be produced to drawing — contact us for samples or a quotation.
Specifications across this series
4 parts in this series
| Part | Finish Code | Environmental Gr… | Salt Spray Stand… | Appearance / Col… |
|---|---|---|---|---|
| Black Nickel · TZ012 / REACH / RoHS compliant / 12-48 h; sealing treatment extends protection | TZ012 | REACH / RoHS compliant | 12-48 h; sealing treatment extends protection | Matt black |
| Chrome Plating (Bright Chrome) · TZ013 / Trivalent chromium decorative plating, RoHS compliant / 48-120 h; increases with nickel layer thickness | TZ013 | Trivalent chromium decorative plating, RoHS compliant | 48-120 h; increases with nickel layer thickness | Mirror-bright chrome |
| Plating () · TZ019 / REACH / RoHS compliant / 24-72 h; longer with increased plating thickness | TZ019 | REACH / RoHS compliant | 24-72 h; longer with increased plating thickness | Bright, mirror-like |
| Zinc plated · TZ020 / Trivalent chromium passivate available. RoHS compliant / 240 h; higher specification available on request | TZ020 | Trivalent chromium passivate available. RoHS compliant | 240 h; higher specification available on request | Matt silver |
Values are taken from each part’s own attribute set. Changing length, material or finish changes pull-out strength and installation torque, so compare the row that matches your drawing.
Selection and test data: engagement length, standards, salt-spray hours
FAQ
What does this finish provide?
Finish Code TZ013, Environmental Grade Trivalent chromium decorative plating, Salt Spray Standard 48-120 h, Appearance / Colour Mirror-bright chrome.
How does it affect torque and friction?
Carbon Steel.
What should I verify before ordering or installing it?
Quote the standard, the hours and the acceptance criterion together — a salt-spray figure without the test method is not a specification. Check that the coating process is compatible with the core hardness of the part.